Blog

  • West Africa Case Study: 15 Kales 40ft Flatbed Trailers, Zero Frame Cracks in 12 Months

    West Africa Case Study: 15 Kales 40ft Flatbed Trailers, Zero Frame Cracks in 12 Months

    Customer Case Study · West Africa · 2025

    How a West African fleet went from 4 frame cracks to zero failures with 15 Kales 40ft flatbed trailers

    In early 2025, a West African logistics operator approached Kales after repeated failures across its trailer fleet. Four out of ten trailers from a previous supplier developed main beam cracks in less than 12 months, and corrosion had already begun shortening chassis life.

    Twelve months after switching to 15 Kales 3-axle 40ft flatbed semi-trailers with Q355 steel chassis and full electrostatic powder coating, the fleet reported zero structural failures, 99%+ uptime, and a clear repeat-order intent. This case study shows how the right specification changes the result on the ground.

    Project Summary

    • Fleet size: 15 units of 3-axle 40ft flatbed semi-trailers
    • Region: West Africa
    • Original issue: 4 frame cracks across 10 previous trailers within 12 months
    • Kales upgrade: Q355 chassis, robotic welding, electrostatic powder coating
    • 12-month result: zero structural failures and 99%+ uptime
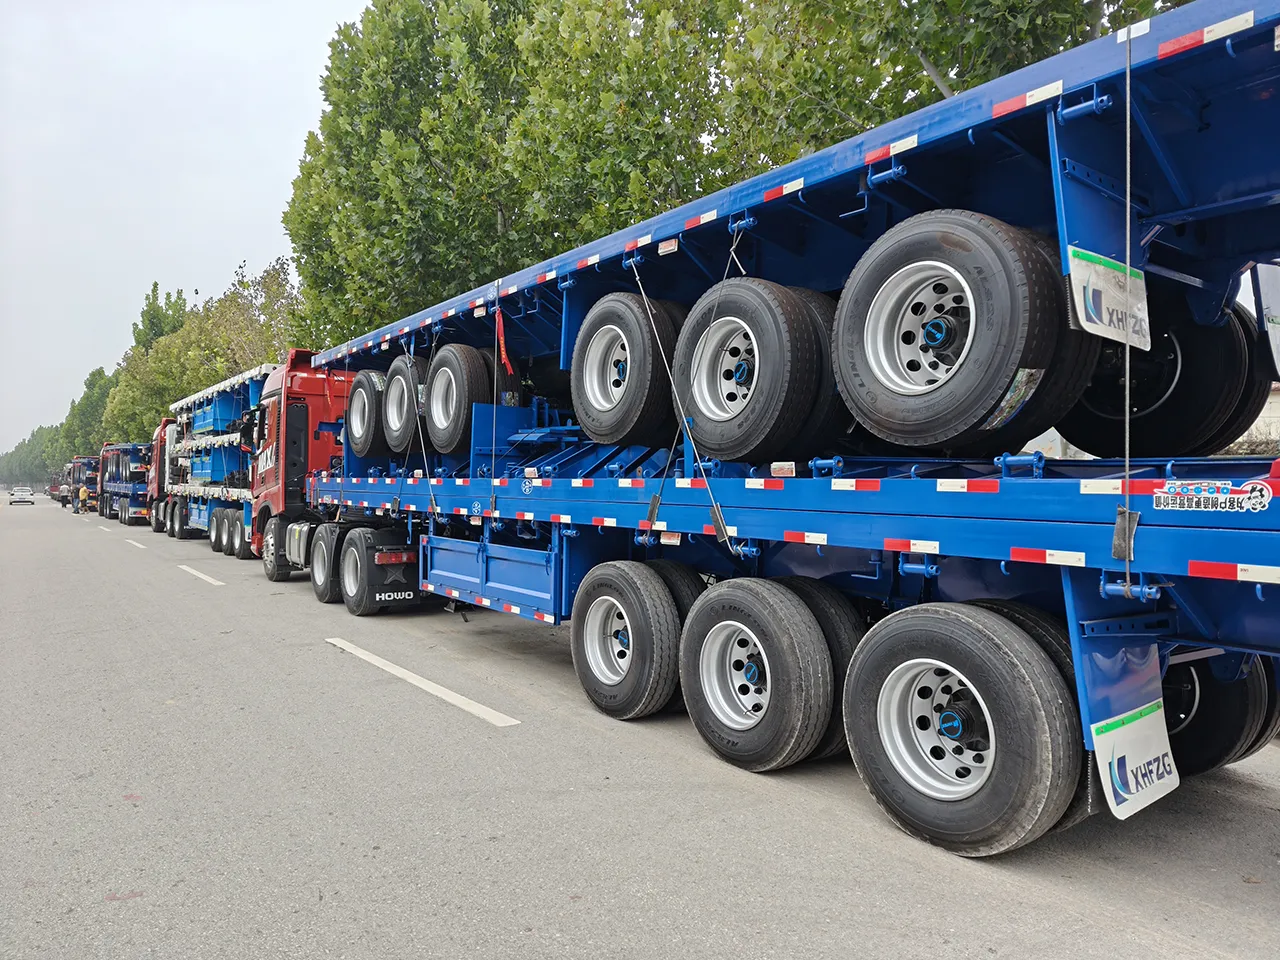
    15 Kales 3-axle 40ft flatbed trailers loaded before shipment to West Africa
    The full 15-unit batch staged before shipment from Tianjin Port. Pre-shipment photos helped the customer confirm quantity, configuration, finish quality, and export readiness before ocean transport to West Africa.

    How to Read This Case

    This article is based on a real 15-unit flatbed trailer delivery and 12-month customer feedback. The customer name is withheld, but the operating profile, failure pattern, trailer configuration, pre-shipment photos, and acceptance-inspection context are retained so fleet buyers can evaluate the specification logic.

    • Evidence used: delivery batch photos, reported previous-fleet failures, and 12-month operating feedback
    • Decision focus: chassis steel, weld consistency, coating system, payload use, and local maintenance access
    • Limit: results depend on payload discipline, road conditions, maintenance practice, and local regulation

    Project at a Glance

    Client Logistics and haulage company in West Africa
    Challenge Previous trailers from another supplier suffered main beam cracks and premature corrosion within 12 months, causing repeated downtime on core haulage routes.
    Solution 15 x Kales 3-axle 40ft flatbed semi-trailers with Q355 high-strength steel chassis, robotic welding at critical joints, and full electrostatic powder coating.
    Outcome All 15 units stayed operational with zero structural failures after 12 months, supporting 99%+ uptime and a strong basis for repeat purchasing.

    Client Operating Profile

    The customer operates a mixed-route haulage fleet serving port, construction, and inland logistics work across West Africa. To keep the buyer anonymous while still making the context useful, this case is best understood as a West African corridor application similar to Nigeria, Ghana, Cote d’Ivoire, Senegal, Togo, and Benin. Their trailers regularly carry containers, bulk cargo, steel products, construction materials, and palletized loads on routes where humidity, road surface quality, and loading practices vary from trip to trip.

    Operating Region West Africa, with conditions similar to port and inland routes in Nigeria, Ghana, Cote d’Ivoire, and Senegal
    Typical Cargo Containers, steel, construction materials, bulk cargo, and general heavy freight
    Main Buying Concern Avoiding repeated frame cracks, corrosion damage, and downtime after previous low-cost trailers failed early
    Fleet Goal Standardize on a stronger 40ft flatbed trailer platform suitable for 40-50 ton logistics work

    The Problem: Why Their Previous Trailers Failed

    The client’s previous trailers, sourced from a low-cost supplier, used inadequate Q235 mild steel for the main beam, a common cost-cutting practice in budget trailer manufacturing. Combined with single-pass manual welding and a thin layer of conventional wet paint, the units were not suited to sustained West African operating conditions.

    Four operating stressors pushed the old fleet into early failure:

    • Tropical humidity accelerating corrosion under thin paint films
    • High operating temperatures reducing fatigue tolerance under load
    • Heavy mineral and aggregate cargoes pushing axle loads close to design limits
    • Long-distance highway and cross-border runs across demanding regional corridors

    Failure Inspection Findings

    Before recommending a replacement specification, Kales reviewed the customer’s reported failure pattern. The damage was not limited to surface rust. The previous trailers showed structural fatigue symptoms in the areas that usually carry the highest stress during heavy flatbed operation.

    • Main beam fatigue: cracks appeared after repeated heavy loading and long-distance operation.
    • Suspension bracket stress: local stress concentration increased under rough-road vibration.
    • Coating breakdown: thin wet paint allowed corrosion to spread around weld seams and underside surfaces.
    • Inconsistent weld quality: variable weld penetration increased the risk of early cracking around critical joints.

    This diagnosis shaped the final trailer specification: stronger steel for the main structure, more consistent welding for high-stress zones, and a more durable coating system for humid and coastal conditions.

    The Hidden Cost of Trailer Frame Failure

    For heavy-duty logistics operators, a cracked trailer frame creates more cost than the welding repair itself. Every failed trailer can remove capacity from the schedule, delay cargo movement, increase driver waiting time, and force the company to rent substitute equipment during peak demand.

    • Direct repair cost: welding, reinforcement, repainting, and workshop labor
    • Downtime cost: trailer unavailable for dispatch while repairs are completed
    • Replacement capacity cost: rented trailers or outsourced transport
    • Operational risk: delayed delivery, missed cargo windows, and reduced customer confidence
    • Future resale impact: visible frame repair can reduce second-hand trailer value

    The Kales Solution: Engineered for West African Conditions

    Kales reviewed the failure pattern and proposed a 15-unit build focused on three upgrades over common market specifications. Each upgrade was selected to answer a known failure mode from the client’s previous fleet.

    This configuration was based on the same heavy-duty platform used in the Kales 3-axle 40ft flatbed trailer for Africa, with adjustments made for the customer’s cargo profile, road conditions, and maintenance expectations.
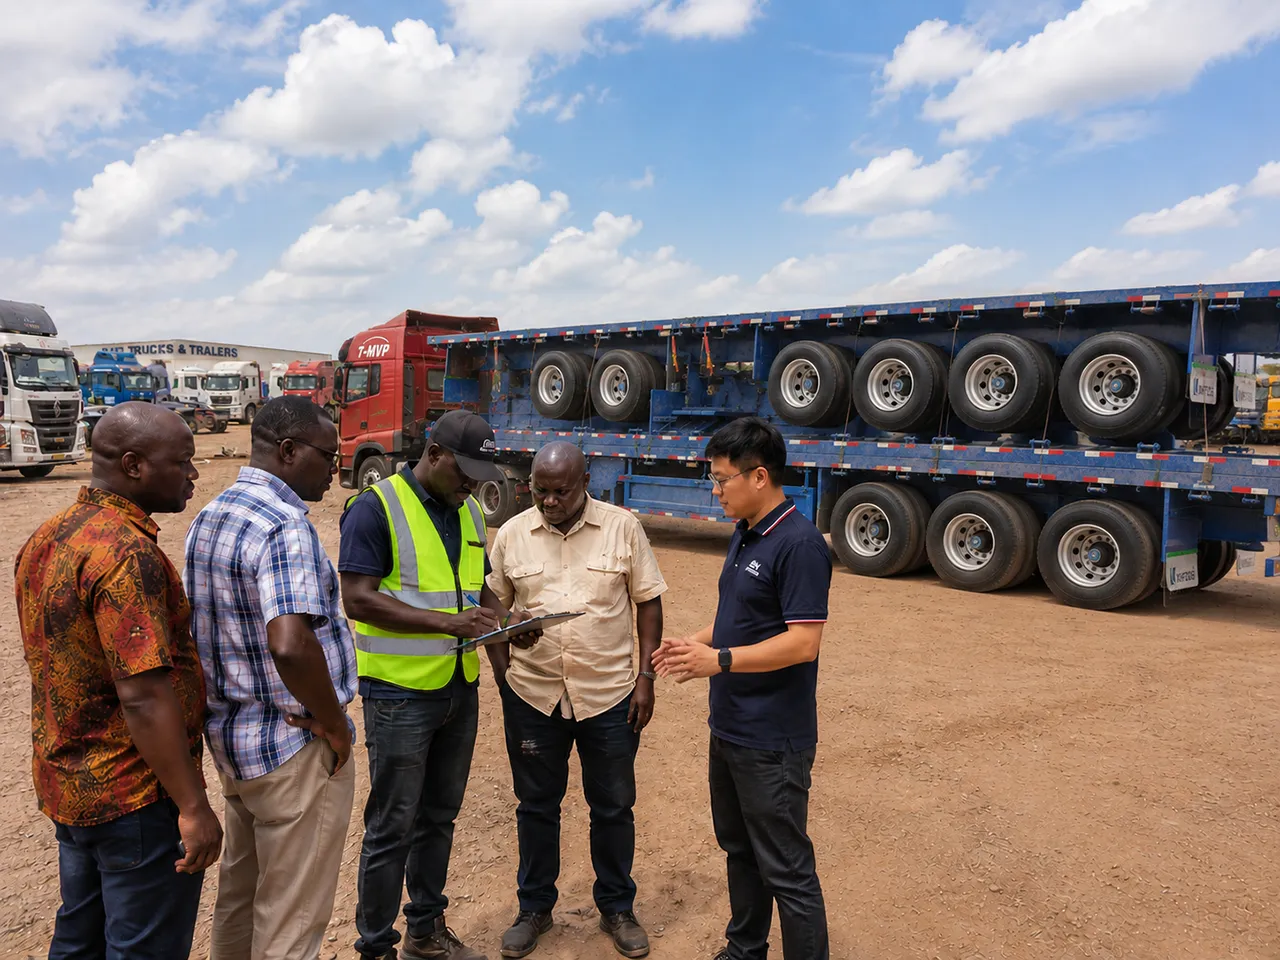
    Customer acceptance inspection of Kales flatbed trailers in West Africa
    Arrival-side acceptance inspection focused on chassis finish, structural alignment, suspension installation, brake system layout, and overall configuration accuracy before the units entered regular service.

    1. Q355 High-Strength Steel Chassis

    Compared with Q235 mild steel commonly seen in budget trailers, Q355 high-strength low-alloy steel provides stronger yield strength, better fatigue resistance under cyclic loading, and better performance in critical stress-concentration areas such as the kingpin section and suspension brackets.

    2. Robotic Welding for Critical Joints

    All structural welds at high-stress locations, including the kingpin assembly, suspension bracket connections, and main beam intersections, were completed using robotic welding rather than variable manual welding. This improves penetration consistency, reduces porosity risk, and keeps quality uniform across the full batch.

    3. Three-Stage Electrostatic Powder Coating

    Surface protection in tropical and coastal environments requires more than wet paint. Kales applied a three-stage coating process designed for long service life in corrosive duty cycles:

    Step Process Benefit
    1 Sandblasting to remove scale, impurities, and rust Maximizes coating adhesion to the steel surface
    2 Full electrostatic powder coating over the chassis Creates an even protective layer with no thin spots
    3 High-temperature baking at 200°C in an industrial oven Hardens the coating shell against scratches, UV, and salt corrosion

    Versatile Cargo Handling: Containers and Bulk Freight

    For logistics fleets in West Africa, trailer utilization matters as much as chassis strength. The customer needed a flatbed platform that could handle container moves, construction materials, bagged freight, timber, steel products, and return-trip freight without changing trailer type.

    • Container ready: 12 twist locks for 1 x 40ft or 2 x 20ft ISO containers
    • Anti-slip floor: 3mm checkered steel plate to reduce cargo shifting
    • Bulk cargo ready: 20 rope tighteners to secure bagged cement, timber, steel bars, and other mixed freight
    Feature Configuration Fleet Benefit
    Container ready 12 twist locks for 1 x 40ft or 2 x 20ft ISO Faster port-to-inland container transport with easier loading and unloading
    Bulk cargo 20 rope tighteners along the side beams Secures cement bags, timber, steel bars, and mixed return freight
    Flat deck 3mm textured steel deck Reduces slippage and protects the chassis from moisture

    Why This Specification Was Chosen

    For West African fleets, the right choice is not simply the cheapest trailer. The platform must tolerate variable payloads, tropical humidity, feeder roads, long-distance highway cycles, and repeated loading without turning welds or suspension brackets into recurring repair points.

    The customer chose this configuration because it balanced payload, strength, serviceability, and export cost. Kales focused the investment where the service-life impact is strongest: chassis steel, weld consistency, suspension durability, brake reliability, and anti-corrosion protection.

    Delivery and Commissioning

    1. Pre-shipment inspection: welds, chassis, paint finish, and equipment compliance were checked before export.
    2. Export documentation: commercial invoice, packing list, bill of lading, technical sheet, and warranty were prepared for customs and fleet records.
    3. Arrival acceptance: the customer inspected the configuration, finish, and operating readiness before the units entered service.

    12-Month Performance Results

    After 12 months of continuous service, the difference from the previous fleet was clear.

    Metric Before After Kales
    Structural failures in year 1 4 incidents across 10 units 0 incidents across 15 units
    Average repair cost per year about $6,000 per fleet $0 structural repair cost
    Fleet uptime about 82% 99%+
    Estimated 3-year repair savings — $18,000+

    The improvement came from changing the specification standard, not just replacing old trailers with new ones. Moving to a Q355-based heavy-duty platform reduced repeat frame repair risk, protected dispatch capacity, and created a clearer reference for future procurement.
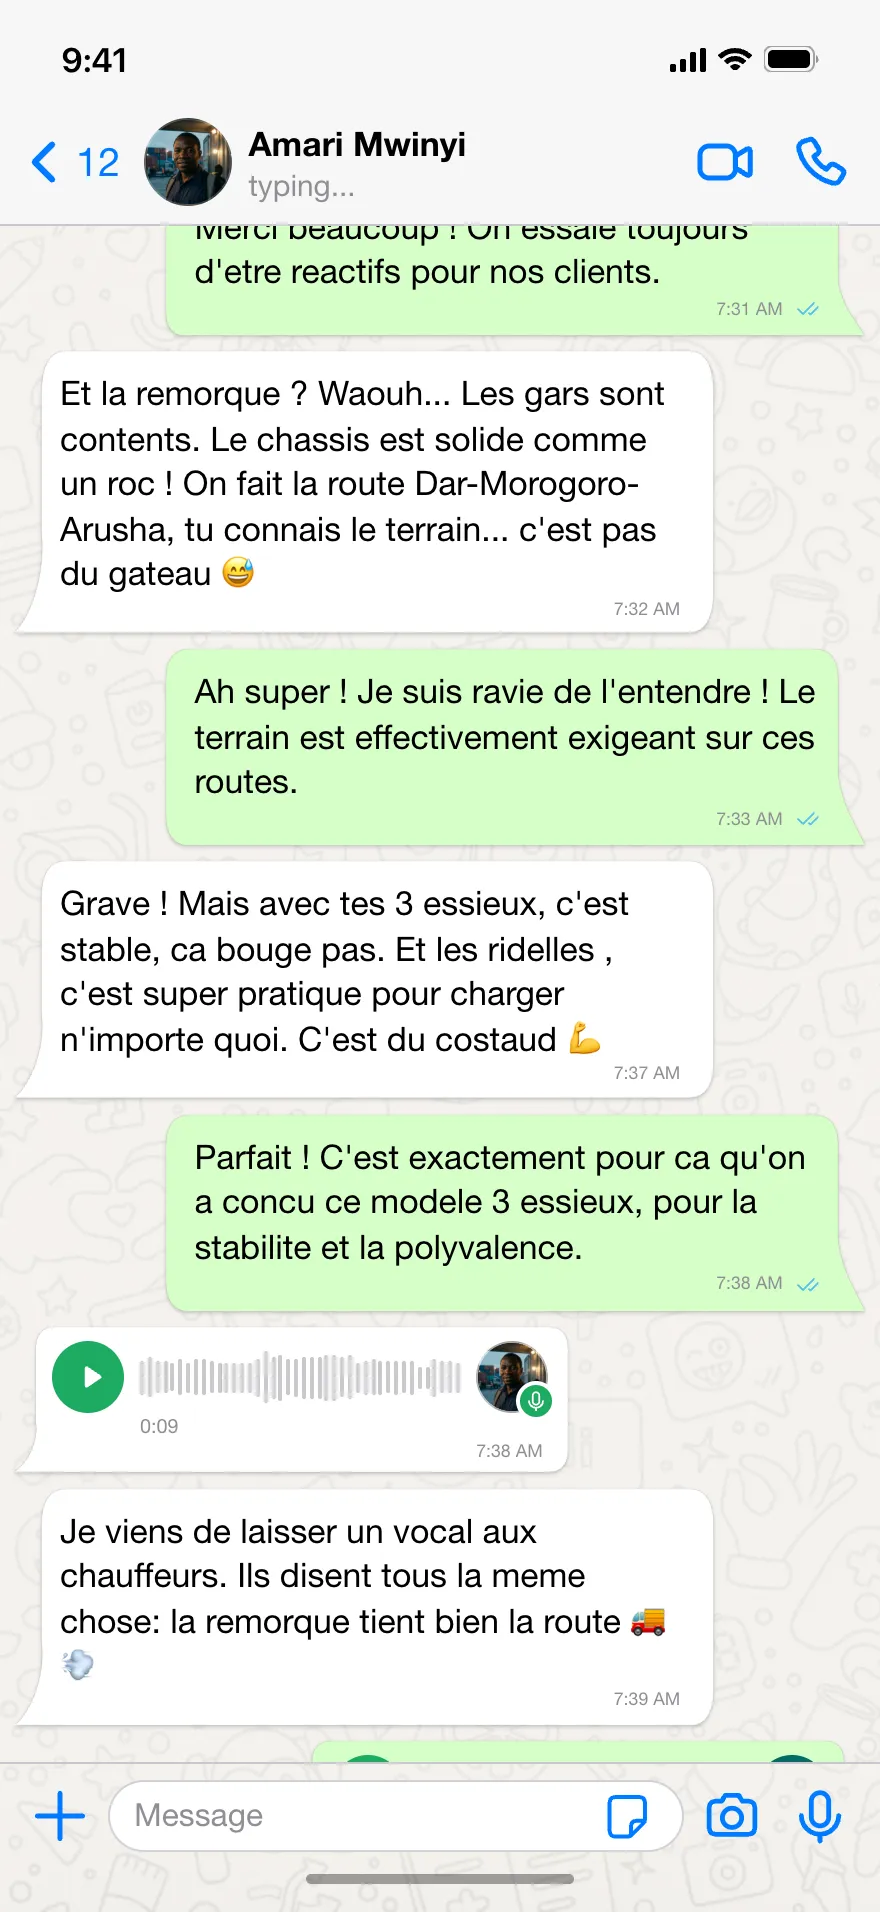
    Customer WhatsApp feedback on Kales flatbed trailer quality and after-sales support
    Customer follow-up feedback after delivery helped confirm that the trailer specification, finish quality, and after-sales communication met the fleet’s expectations for future orders.

    The ROI story

    Beyond avoided repair costs, the larger gain came from uptime. More reliable fleet availability improved route continuity, reduced substitute transport spending, and strengthened the case for continuing with a higher-spec trailer platform.

    Operational Impact After 12 Months

    • Dispatch reliability improved: fewer unexpected trailer withdrawals from daily planning
    • Maintenance became more predictable: inspections focused on routine wear parts instead of structural repair
    • Driver confidence improved: stronger chassis and stable braking reduced concern on loaded routes
    • Procurement risk decreased: the customer now has a proven specification for future fleet expansion

    Recommended Specification for Similar West African Fleets

    For buyers operating in West Africa, Kales recommends choosing trailer specifications according to cargo weight, road quality, corrosion exposure, and maintenance capability. A low purchase price may look attractive at first, but weak chassis materials and poor coating quickly increase total ownership cost.

    Operating Scenario Recommended Configuration Reason
    General logistics and container work 3 axles, 13-ton axles, mechanical suspension, Q355 chassis Balanced for payload, cost, and serviceability
    Mining or aggregate transport Reinforced beam, 16-ton axle option, heavy-duty leaf spring suspension Improves resistance to high payload and rough-road impact
    Coastal or humid operation Sandblasting plus electrostatic powder coating Reduces corrosion around weld seams and underside surfaces
    Long-distance cross-border routes Branded brake system, reliable landing gear, common tire size Makes maintenance easier across regional workshops

    What Other West African Fleet Operators Should Take Away

    1. Material grade matters more than sticker price. Lower upfront cost can quickly be erased by beam repairs and downtime.
    2. Surface protection defines service life in humid climates. A proper coating process is a structural decision, not a cosmetic one.
    3. Welding consistency matters on heavy-duty routes. Stable weld quality is essential for long-distance, high-payload use.

    Buyer Checklist Before Ordering Flatbed Trailers for Africa

    Before ordering a new batch of flatbed semi-trailers, fleet owners should confirm the operating conditions clearly. These details help Kales recommend the right model and avoid under-specification.

    • Target cargo: container, steel, cement, aggregate, equipment, or mixed freight
    • Expected payload: normal working load and maximum occasional load
    • Road condition: highway, port road, mining road, rural feeder road, or mixed route
    • Climate exposure: coastal humidity, rainy season operation, dust, or salt air
    • Maintenance access: preferred axle, tire, brake, and landing gear brands available locally
    • Shipping destination: target country, port, inland delivery point, and preferred delivery schedule

    Frequently Asked Questions

    What is the load capacity of a Kales 3-axle 40ft flatbed trailer?

    The standard configuration carries up to 50 tons of payload using 3 x 13-ton heavy-duty axles. For mining and aggregate work, a 16-ton axle upgrade is available depending on the tractor and local road regulations.

    How long does shipping take from China to West Africa?

    Container shipping to Lagos, Tema, Abidjan, or Dakar typically takes 30-38 days. RoRo shipping for fully assembled units can take a little longer depending on the route and vessel schedule.

    What documentation is provided with each trailer?

    Each unit ships with a certificate of origin, commercial invoice, packing list, bill of lading, manufacturer specification sheet, and a 12-month structural warranty certificate. Customs clearance assistance is available for regular destination markets.

    Are spare parts available locally in West Africa?

    Yes. Kales maintains spare-parts arrangements with partners in Lagos, Tema, Abidjan, and Dakar. Branded components such as BPW axles, JOST landing gear and kingpins, and WABCO brakes are also widely serviceable at independent workshops across the region.

    What is the warranty on Kales flatbed trailers?

    The standard warranty covers the chassis structure and main welds for 12 months, electrical and hydraulic components for 6 months, plus pass-through warranties from branded suppliers such as BPW, JOST, and WABCO under their original terms.

    Can the trailer specifications be customized?

    Yes. Length, axle count, kingpin size, suspension type, tire size, and brake configuration can all be adjusted. Minimum order quantity for custom configurations is typically 5 units.

    Which flatbed trailer model was used in this West Africa case?

    The project used a customized version of the Kales 3-axle 40ft flatbed semi-trailer for Africa, configured with Q355 steel, heavy-duty axles, mechanical suspension, JOST-compatible kingpin options, and electrostatic powder coating for humid and high-load operating conditions.

    Why is Q355 steel better than Q235 for heavy-duty flatbed trailers?

    Q355 steel has higher yield strength than Q235 mild steel, which helps the main beam resist bending and fatigue under repeated heavy loads. For fleets carrying containers, aggregate, steel, or construction materials, Q355 is usually a better choice for long-term chassis durability.

    Is electrostatic powder coating necessary for West African trailer operation?

    For humid, coastal, or rainy-season operation, electrostatic powder coating gives stronger and more even protection than basic wet paint. It is especially useful around weld seams, chassis underside areas, and structural edges where corrosion usually starts first.

    Need a flatbed trailer spec for West African routes?

    Share your cargo type, target payload, road conditions, and destination port. Kales will recommend the right 3-axle 40ft flatbed trailer configuration for your fleet.

    View Trailer Specification
    Request a Fleet Quote

    Published by: Kales Truck Engineering Team

    Last updated: May 21, 2026 | Published: May 21, 2026

    Related: 3-Axle 40ft Flatbed Trailer for Africa · All Semi Trailers · Request a Quote
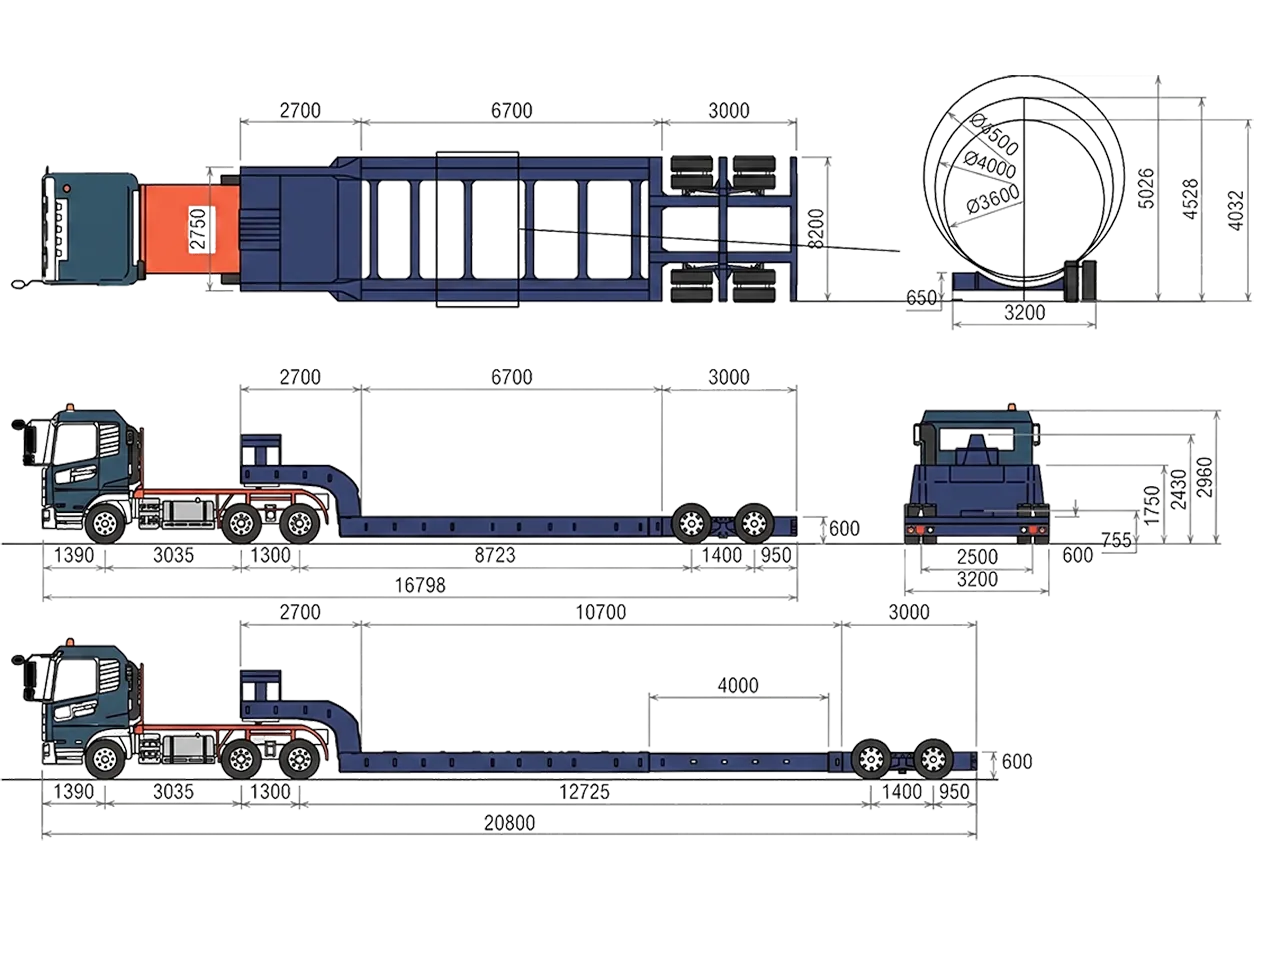
  • How to Measure a Tractor Truck for Semi-Trailer Matching

    How to Measure a Tractor Truck for Semi-Trailer Matching

    Published: May 18, 2026 | Last updated: May 30, 2026

    Technical Guide by Kales Vehicle

    How to Measure Your tractor truck for the Perfect Semi-Trailer Match

    The complete guide to 4 critical measurements that ensure your custom trailer fits flawlessly — from fifth wheel height to axle load distribution.

    Quick Answer: To order a custom semi-trailer that perfectly matches your tractor, you need four measurements: (1) Fifth Wheel Height (H) — ground-to-coupling-plate distance (standard: ≤1,400mm unladen); (2) Rear Swing Radius (R2) — king pin to tractor rearmost point (≤2,200mm); (3) Front Clearance Radius (R1) — king pin to nearest cab-rear obstruction (≥150mm clearance); (4) Fifth Wheel Setback (Fx) — fifth wheel pivot to rear axle center. All must be actual tractor measurements on flat ground — not manufacturer specs.

    Measurement Method and Scope

    This guide is written for export buyers who need Kales to confirm tractor-trailer compatibility before production. It does not replace the tractor manufacturer’s engineering data, but it gives procurement teams, workshop managers, and drivers a practical field method for recording the dimensions that affect trailer design.

    • Use it for: flatbed trailers, lowbed trailers, tanker trailers, container chassis, and other custom semi-trailers
    • Record together: fifth wheel height H, rear swing radius R2, front clearance radius R1, and fifth wheel setback Fx
    • Send with photos: side view, rear chassis view, fifth wheel close-up, and any CNG, LNG, hydraulic, or battery equipment behind the cab

    Why Tractor-Trailer Matching Matters More Than You Think

    A semi-trailer has no driving power of its own — it relies entirely on the tractor truck for traction, steering, and braking. This means the trailer must be engineered around your specific tractor’s dimensions, not built as a one-size-fits-all product.

    At Kales Vehicle, we’ve seen what happens when tractor-trailer matching goes wrong: premature tire wear, axle overload, suspension failure, poor steering, and even dangerous jackknifing. Every one of these problems is preventable — if you provide the right measurements before production begins.

    # Parameter Symbol Why It Matters
    1 Fifth Wheel Height H Cargo platform height & suspension selection
    2 Rear Swing Radius R2 Gooseneck design & landing gear placement
    3 Front Clearance Radius R1 Front overhang & cab-to-trailer gap
    4 Fifth Wheel Setback Fx Axle load distribution
    Important: All four parameters are mandatory for custom trailer design. Missing even one makes proper design impossible.

    Before You Measure: Record the Tractor Configuration

    Before measuring dimensions, write down the tractor model, wheelbase, fifth wheel model, tire size, suspension type, and any rear-cab equipment. These details explain why two tractors with similar horsepower can require different trailer neck height, kingpin position, landing gear position, or front clearance.

    Item to record Why it matters
    Fifth wheel model and height Sets trailer front height and keeps the deck level under load.
    Rear-cab equipment CNG tanks, LNG tanks, battery boxes, hydraulic tanks, and toolboxes can reduce turning clearance.
    Suspension and tire size Ride height changes with tire and suspension choices, especially on rough-road export configurations.

    1. Fifth Wheel Height (H) — The Foundation of Every Trailer Design

    What Is Fifth Wheel Height?

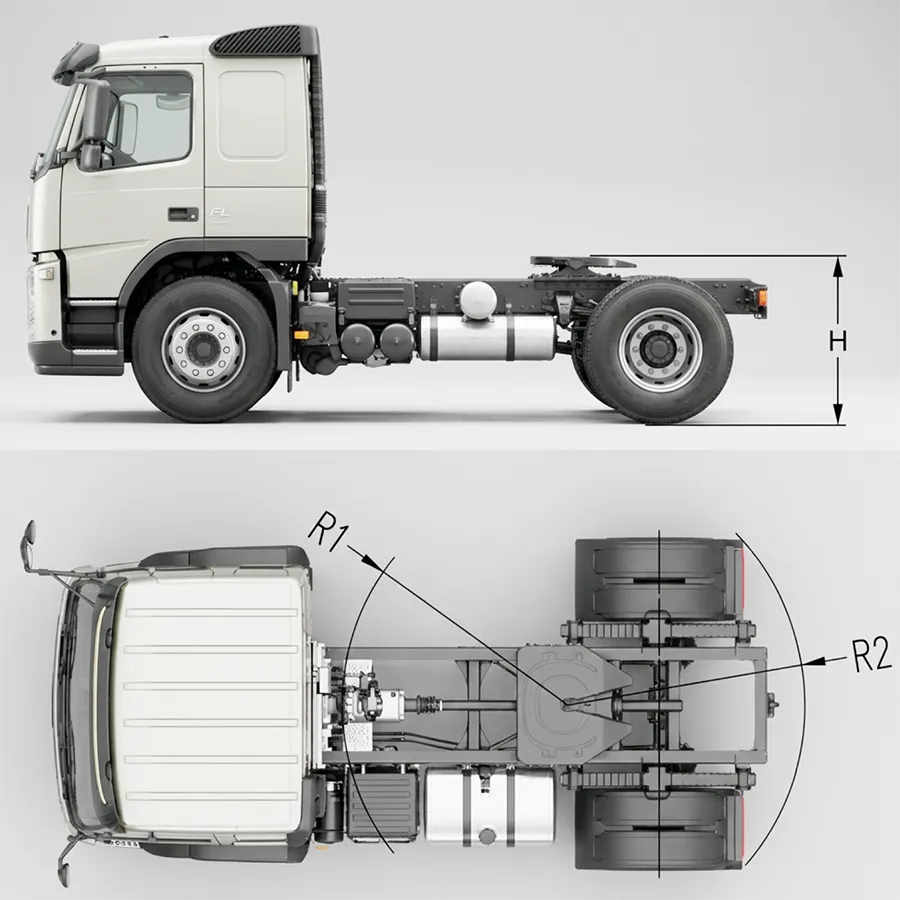
    The fifth wheel height (also called saddle height or coupling height) is the vertical distance from the ground to the top surface of the fifth wheel coupling plate when the tractor is parked on level ground and the fifth wheel is in its horizontal position.

    There are two types: Unladen (empty) — measured with no trailer connected, and Laden (loaded) — measured under full load.

    Tip: When ordering from Kales Vehicle, always report the unladen (empty) fifth wheel height. This is the standard reference for trailer design.
    Semi truck measurement positions for fifth wheel height H, rear swing radius R2, and front clearance radius R1
    Measurement reference for fifth wheel height H, rear swing radius R2, and front clearance radius R1.

    Why Fifth Wheel Height Is Critical

    • Determines the cargo platform height (loading height)
    • Dictates the suspension type and ride height
    • Directly affects axle load distribution between tractor and trailer
    • Without this measurement, no trailer can be designed

    How to Measure – Step by Step

    Tools: Straight ruler or steel tape measure (min. 1.5m / 5ft)

    1. Park your tractor on a hard, flat, level surface (concrete or asphalt)
    2. Ensure the fifth wheel plate is in its horizontal (level) position
    3. Measure the vertical distance from the ground to the highest point on the fifth wheel plate top surface
    Record in millimeters (mm). A difference of just 10–15mm can significantly impact performance.

    Industry Standards

    Condition Max Height
    Standard unladen tractor ≤ 1,400 mm
    For 8’6″ (2,591mm) ISO containers ≤ 1,320 mm
    For 9’6″ (2,896mm) high-cube containers ≤ 1,110 mm
    Laden (general semi-trailer, excl. skeleton) 1,150 – 1,300 mm

    What Happens When Height Is Wrong?

    Warning: Fifth Wheel TOO HIGH:

    • Trailer front axle load decreases → front tires wear flat
    • Tractor fifth wheel position overloaded → understeer
    • Tractor may wheelie on inclines

    Warning: Fifth Wheel TOO LOW:

    • Trailer rear axle load decreases → rear tires wear flat
    • Front axle overloaded → tire blowouts, shoulder wear
    • Front axle leaf springs may crack or deform
    • Tractor drive wheels lose traction, may spin
    Kales Vehicle Recommendation: Keep matching deviation within +10mm (upper) and -15mm (lower). We calibrate every trailer’s front-end height to your exact fifth wheel measurement.

    2. Rear Swing Radius (R2) — Preventing Tractor-Trailer Collision

    What Is Rear Swing Radius?

    The rear swing radius (R2) is the horizontal distance from the center of the fifth wheel king pin hole to the rearmost point of the tractor — measured as a projected distance on the ground plane. When the tractor turns sharply, the rear end swings outward — R2 tells us how far back the tractor extends behind the coupling point.

    Why It Matters

    • Determines the gooseneck transition dimensions
    • Determines landing gear placement position
    • Too large R2 creates interference during turns

    How to Measure – Step by Step

    Tools: Steel tape measure (min. 3m / 10ft)

    1. Park your tractor on a hard, flat, level surface
    2. Measure the horizontal distance from the king pin hole center to the rearmost point of the tractor chassis or body
    Guideline Value
    Max recommended R2 (swap-body operations) ≤ 2,200 mm
    Min clearance: tractor rear ↔ trailer gooseneck 70 – 100 mm
    Warning: If R2 is reported smaller than actual, the trailer gooseneck may collide with the tractor’s rear chassis, bumper, or air tanks during sharp turns.
    Kales Vehicle Recommendation: Smaller R2 values are generally better for design flexibility. We design every gooseneck with 70–100mm clearance, but need your accurate R2 to do this correctly.

    3. Front Clearance Radius (R1) — Protecting Cab-Mounted Equipment

    What Is Front Clearance Radius?

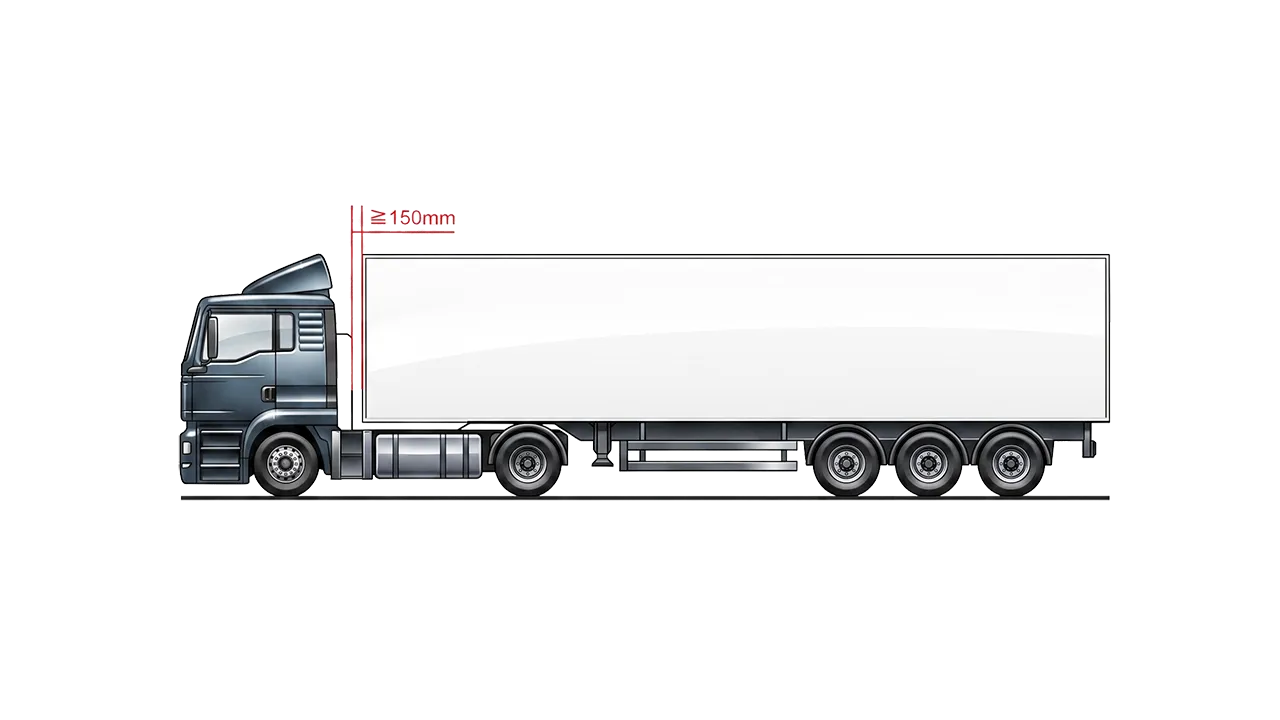
    The front clearance radius (R1) is the horizontal distance from the center of the fifth wheel king pin hole to the nearest obstruction behind the cab — measured on the Y-plane (lateral vertical plane).

    Common obstructions include: air filter housings, CNG/LNG gas cylinders, battery boxes, exhaust aftertreatment systems (SCR, DPF), and hydraulic tanks.

    Why It Matters

    • Determines the front overhang design of the trailer
    • Prevents trailer front from colliding with cab equipment during turns
    • Especially critical for CNG, LNG, and electric tractors with large equipment behind the cab

    How to Measure – Step by Step

    Tools: Steel tape measure (min. 3m / 10ft)

    1. Park your tractor on a hard, flat, level surface
    2. Identify the closest obstruction behind the cab
    3. Measure horizontal distance from king pin center to this nearest point, along the Y-plane
    Guideline Value
    Typical R1 range ≤ 2,040 + 150 mm
    Min clearance: trailer front ↔ tractor cab equipment ≥ 150 mm
    Caution — CNG/LNG/Electric Tractors: These vehicles often have significantly reduced R1 values due to large gas cylinder racks or battery packs. Failure to report accurately can result in the trailer striking expensive fuel system components.

    What Happens When R1 Is Wrong?

    • R1 too large / trailer too short: Excessive gap → aerodynamic drag, wider turning radius, instability, possible overlength
    • R1 too small / trailer too long: Front-end collision → may rupture gas cylinders or damage electrical systems
    Kales Vehicle Recommendation: We pay special attention to front clearance for CNG/LNG and electric tractors, increasingly common in Africa, Middle East, and Latin America. Send a photo of your tractor’s rear-cab area alongside the R1 measurement.

    4. Fifth Wheel Setback (Fx) — The Key to Axle Load Distribution

    What Is Fifth Wheel Setback?

    The fifth wheel setback (Fx) is the horizontal distance from the vertical plane through the fifth wheel pivot axis to the vertical plane through the center of the rear axle(s). In simpler terms: how far forward the fifth wheel sits relative to the rear axle.

    Fifth wheel setback Fx measurement and minimum tractor trailer clearance diagram
    Fifth wheel setback Fx measurement and minimum clearance reference for tractor-trailer matching.

    Why It Matters

    • Critical for axle load distribution calculations
    • Determines how much weight each axle carries when loaded
    • Incorrect Fx causes dangerous driving conditions

    How to Measure – Step by Step

    Tools: Straight ruler or tape measure (min. 2m / 6.5ft)

    1. Park your tractor on a hard, flat, level surface
    2. Measure horizontal distance from king pin center to rear axle center (or midpoint between tandem axles)

    What Happens When Fx Is Wrong?

    Warning: Fx TOO LARGE (fifth wheel too far forward):

    • Rear axle load decreases, reducing traction
    • Dangerous on 6×2 tractors: drive axle may lose grip → wheel spin on grades
    • Tractor struggles to start on inclines

    Warning: Fx TOO SMALL (fifth wheel too far back):

    • Rear axle load exceeds rated capacity
    • Axles, wheels, leaf springs may deform or fail
    • Tractor experiences front-end lift, steering becomes heavy
    Kales Vehicle Recommendation: Fx directly influences trailer axle positions and load distribution. Unsure how to measure? Send us a side-view photo — our engineering team provides free remote guidance.

    Measurement release gate: approve H, R1, R2 and Fx before trailer drawing freeze

    Tractor-trailer matching should have a release gate before the trailer drawing is frozen. The buyer should submit measured fifth wheel height H, rear swing radius R2, front clearance radius R1, fifth wheel setback Fx, tire size, suspension type, fifth wheel model, and photos from both sides plus the rear of cab. These records protect the project when the tractor has been modified, fitted with CNG/LNG tanks, battery boxes, hydraulic kits, toolboxes or a non-standard fifth wheel mounting plate.

    The engineering logic is supported by interchangeability references. ISO 1726-1 covers mechanical coupling interchangeability between tractors and semi-trailers for general cargo, ISO 337 defines the 50 semi-trailer fifth wheel coupling pin dimensions, and SAE J701 addresses truck tractor and semitrailer interchange coupling dimensions. These standards do not replace local regulations, but they are a solid basis for a measurement checklist.

    Approve before drawing freeze

    • H measured on level ground with normal tire pressure and working ride height.
    • R1 checked against rear-cab tanks, batteries, toolboxes and hydraulic equipment.
    • R2 checked against chassis tail, mudguards, fifth wheel plate and gooseneck path.
    • Fx reviewed with axle load target, trailer axle group and payload center.

    Block release if found

    • Only factory spec sheet is provided, but tractor tires, suspension or fifth wheel were changed.
    • No rear-cab photos for CNG, LNG, electric or hydraulic tractors.
    • R1/R2 clearance is not checked at the expected steering angle and articulation.
    • Fx is approved without reviewing axle load distribution and legal payload.

    For African mining, container, fuel, bulk and flatbed fleets, this gate prevents expensive rework after the trailer arrives. A small mismatch can cause kingpin lock problems, landing gear interference, cab-equipment damage, poor axle load distribution or an unsafe trailer nose-up/nose-down attitude. Send the measurement package before production, then keep it with the delivery documents for future fleet replacements.

    Your Measurement Checklist

    Before contacting Kales Vehicle, prepare these four measurements:

    Check Parameter Symbol Tools Key Tip
    ☐ Fifth Wheel Height H Tape ≥ 1.5m Measure unladen, flat ground
    ☐ Rear Swing Radius R2 Tape ≥ 3m To the rearmost point
    ☐ Front Clearance Radius R1 Tape ≥ 3m Nearest obstruction behind cab
    ☐ Fifth Wheel Setback Fx Tape ≥ 2m To rear axle centerline
    Always measure the actual tractor, not the spec sheet. Even same make/model tractors differ due to spring pack and mounting plate variations. Real-world measurements are the only reliable data.

    Frequently Asked Questions

    Q: What measurements do I need from my tractor to order a custom semi-trailer?

    You need exactly four measurements: Fifth Wheel Height (H), Rear Swing Radius (R2), Front Clearance Radius (R1), and Fifth Wheel Setback (Fx). These are mandatory — no responsible manufacturer can design a matched trailer without all four. Always measure your actual tractor on flat ground using a steel tape measure.

    Q: What is fifth wheel height and what is the standard range?

    Fifth wheel height is the vertical distance from ground to the top of the coupling plate. Standard unladen height should not exceed 1,400mm. For ISO containers: ≤1,320mm for 8’6″ and ≤1,110mm for 9’6″ high-cube. Loaded range is typically 1,150–1,300mm.

    Q: What happens if my fifth wheel height doesn’t match the trailer?

    A mismatch beyond +10mm (too high) or -15mm (too low) causes serious issues. Too high reduces front axle load causing flat tire wear. Too low overloads the front axle, risking blowouts, spring failure, and loss of drive traction.

    Q: Do I need different measurements for CNG, LNG, or electric tractors?

    The same four measurements apply, but Front Clearance Radius (R1) requires extra attention. Alternative-fuel tractors mount large gas cylinders or battery packs behind the cab, significantly reducing clearance. At Kales Vehicle, we recommend sending photos of the cab rear area alongside measurements.

    Q: Can I use the manufacturer’s spec sheet instead of measuring?

    No. Even tractors of the same make and model vary due to spring pack configurations and mounting plate thickness. Always measure your specific tractor. Kales Vehicle provides free remote guidance via WhatsApp or video call.

    Why Kales Vehicle Takes Matching So Seriously

    At Kales Vehicle, every semi-trailer is designed around your specific tractor.

    • Factory-Direct Engineering: No middleman — your data goes straight to the design table
    • Precision Matching: Every gooseneck angle, suspension height, and landing gear position is calculated for your exact tractor
    • Global Experience: Customers across Africa, Latin America, Middle East, and Central Asia — matched to Mercedes-Benz, Volvo, Scania, HOWO, Shacman, FAW, Dongfeng, and more
    • Remote Assistance: Free measurement guidance via WhatsApp, video call, or photo analysis

    Ready to Get Started?

    Taking accurate measurements is the first step toward a trailer that performs perfectly.

    1. Measure all four parameters
    2. Photograph your tractor (side, rear, behind cab)
    3. Contact Kales Vehicle with measurements & requirements
    4. Receive a custom proposal within 24 hours

    Email: jennylee@kalestruck.com  |  WhatsApp: +86 131 5638 8843

  • Semi-Trailer Painting and Anticorrosion Process Guide

    Semi-Trailer Painting and Anticorrosion Process Guide

    Published: December 31, 2025 | Last updated: May 30, 2026

    A comprehensive evolution of anti-corrosion & environmental compliance. Learn how to distinguish “True Protection” from “Superficial Shine.”

    What is the best anti-corrosion coating for semi-trailers?
    The optimal anti-corrosion system for high-end semi-trailers combines Cathodic Electrodeposition (E-coat) for the chassis to ensure 360° rust prevention in inner cavities, and Electrostatic Powder Coating or Liquid Baking Paint for the upper body to provide UV resistance and zero-VOC environmental compliance. A scientific E-coat system can extend a trailer’s lifespan to over 15 years in harsh environments.

    Technical basis and scope

    How this guide is supported

    This article combines Kales production experience with recognized coating references. The process logic follows Kales trailer workflow: steel surface cleaning, Sa 2.5 blasting, electrophoretic KTL/e-coat primer where full immersion is required, and powder or liquid baking topcoat for exposed parts. It is written for export buyers comparing factory quotations, not as a replacement for a project-specific coating specification.

    The external technical basis is consistent with ISO 12944 corrosion-protection practice for protective paint systems, ISO 8501-1 visual surface-preparation grades, AMPP/SSPC near-white blast-cleaning practice, and industrial coating guidance from coating manufacturers such as PPG on electrocoat and powder systems. Where a fleet operates in coastal, mining, humid, or salt-exposed routes, the buyer should still define the corrosivity class, target service life, surface-preparation grade, dry-film thickness range, and repair procedure in the purchase contract.

    • Use this guide to compare: manual brushing, liquid spray, KTL/e-coat, liquid baking paint, and electrostatic powder coating.
    • Ask suppliers to prove: blasting grade, pretreatment process, curing record, DFT inspection, adhesion test, and salt-spray or coating report when required.
    • Do not compare only color: a glossy surface can still fail early if the steel profile, primer compatibility, or oven curve is wrong.

    I. Introduction: It’s More Than Just “Face Value”

    Many people believe that painting a semi-trailer is simply a matter of spraying on a few coats of topcoat.

    But in reality, the anti-corrosion system of a modern semi-trailer has evolved from primitive manual brushing to sophisticated industrial processes like Cathodic Electrodeposition (E-coat) + Intermediate Coat + Liquid Baking Paint or Electrostatic Powder Coating. A scientifically engineered paint system allows a high-strength steel chassis to serve safely for 15 years under harsh salt spray, snow-melt chemicals, and mud. Conversely, a low-quality coating can lead to structural rust-through in as little as 3 years.

    Against the backdrop of global “Carbon Neutrality” goals and stricter environmental regulations (such as EU REACH), paint is no longer just a cosmetic feature. It is the bottom line of safety, an environmental responsibility, and a core variable in the Total Cost of Ownership (TCO).

    II. Comparison of the Top 5 Coating Systems

    Process Type Principle VOC Emissions Utilization Typical Application
    Manual Brushing Hand-applied alkyd paint High <30% Small workshops, non-standard repairs
    Standard Liquid Spray Air gun spray (Epoxy/PU) Med/High 40–60% Mainstream chassis beams
    Cathodic E-coat (E-coat) Electrical deposition in tank Very Low >95% Full chassis (including inner cavities)
    Liquid Baking Paint High-temp cured topcoat Medium 50–70% High-end finish, Cabins
    Powder Coating Electrostatic adhesion + Melting Zero VOC >98% Box bodies, Fenders, Toolboxes

    ✅ 2025 Industry Trends:

    • Chassis: E-coat has become the standard mainstream solution for high-end trailers.
    • Upper Body/Accessories: Powder coating is rapidly replacing liquid paint, balancing environmental compliance with physical performance.

    III. Deep Dive: E-coat, Liquid Baking & Powder Coating

    (A) Cathodic Electrodeposition (E-coat)

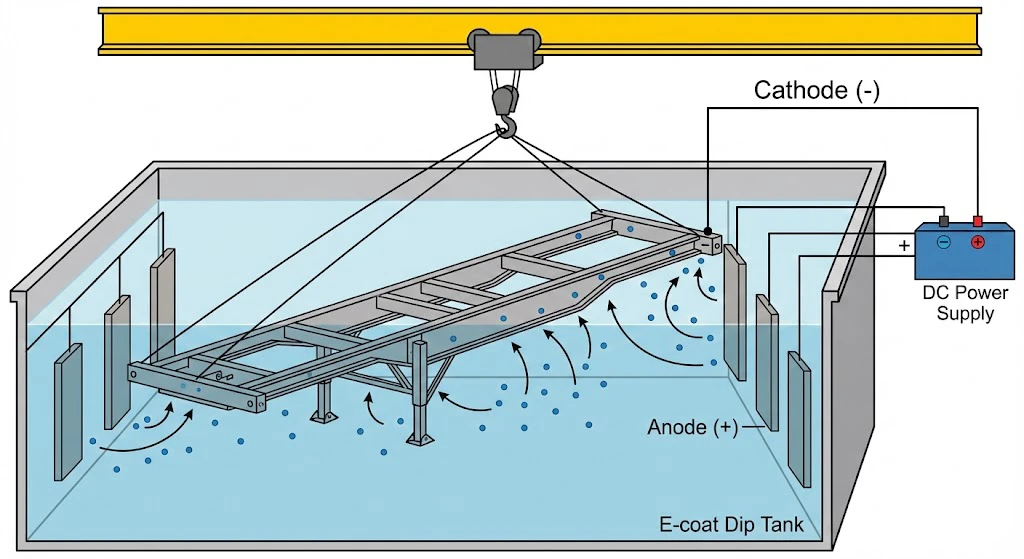
    Diagram illustrating the cathodic electrodeposition (e-coat) process used by Kales Vehicle for semi-trailer chassis, showing the chassis submerged in a dip tank.

    Fig 1: The mechanism of Cathodic Electrodeposition ensuring 360° coverage.

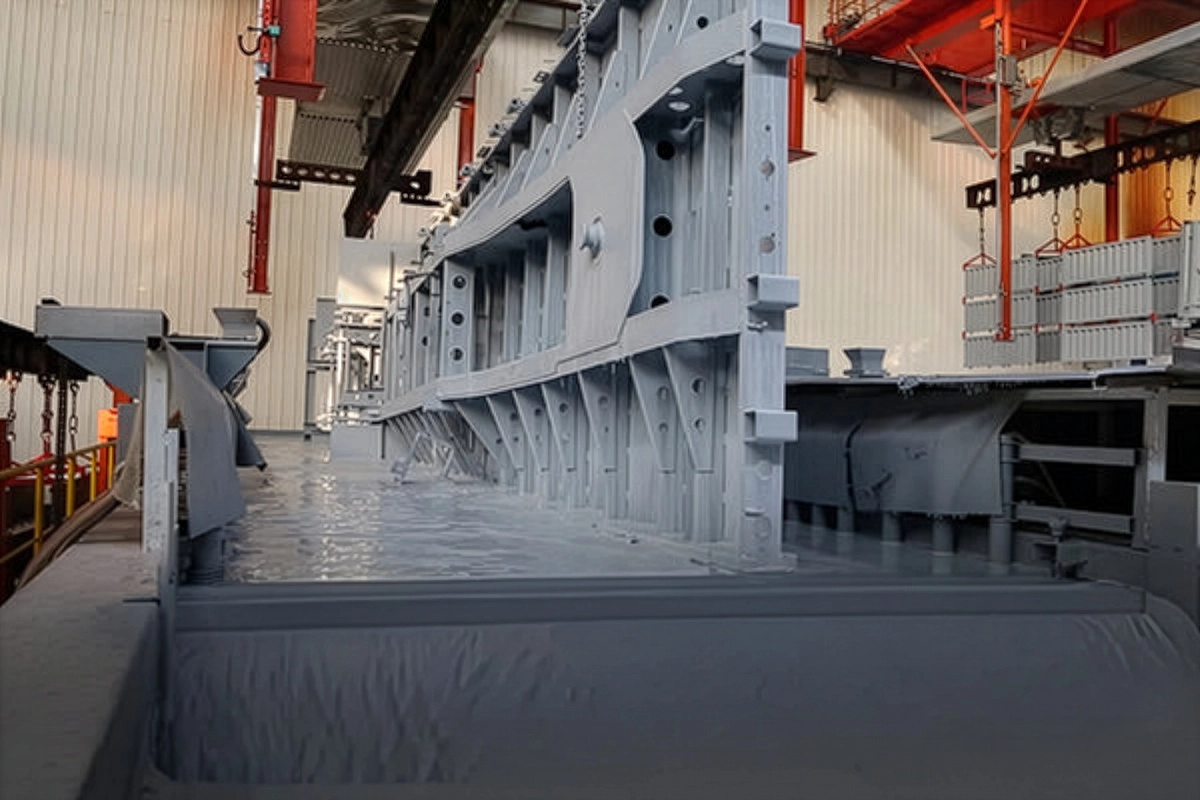
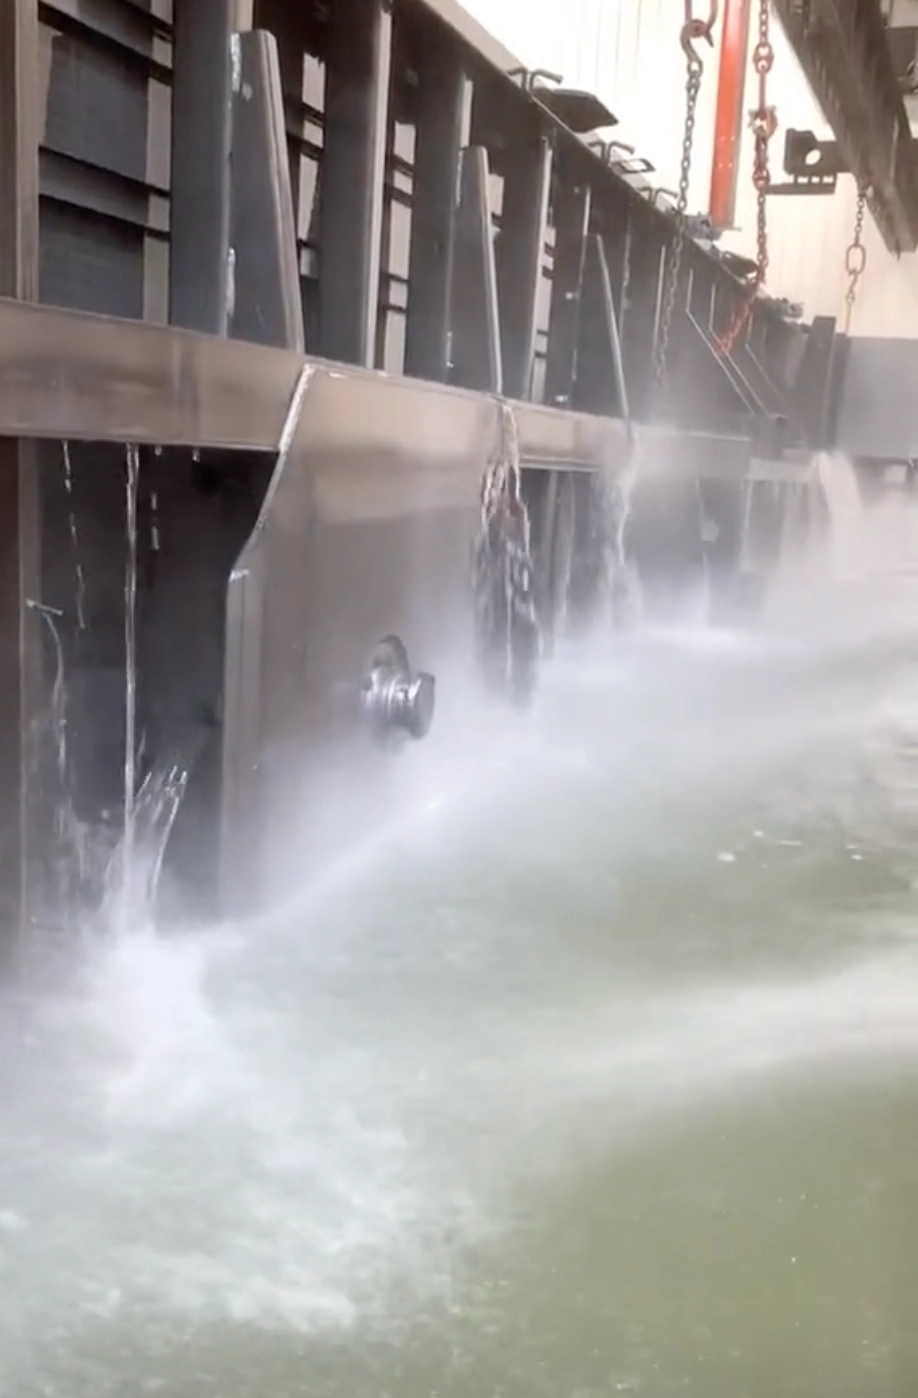
    Kales flatbed semi-trailer frame undergoing electrophoretic coating (e-coat) in a dip tank, ensuring full corrosion protection including inner cavities.Full Immersion Cathodic Electrodeposition (E-coat) reaching all inner cavities at Kales facility.
    • Principle: The entire chassis is submerged in an electrified tank. Paint particles are deposited evenly onto the metal surface, reaching inner cavities and weld seams that spray guns miss.
    • Advantage: 360° coverage, Adhesion Grade 0 (GB/T 9286), Salt Spray Resistance ≥1000 hours with no red rust.
    • ⚠️ Limitations:
      1. High capital investment; strictly for conductive metals.
      2. Poor UV Resistance: E-coat (Epoxy resin) chalks when exposed to sunlight. It must be covered with a UV-resistant topcoat for outdoor use.

    (B) Liquid Baking Paint (High-Temp Cured)

    • Principle: Polyurethane or acrylic resins are cured in baking ovens at 120–140℃, creating a dense cross-linked structure.
    • Advantage: High gloss, excellent color retention (no chalking for 5 years), Pencil Hardness ≥H, resistant to minor scratches.
    • Best For: High-end export trailers, Reefer units, and Aluminum box exteriors.

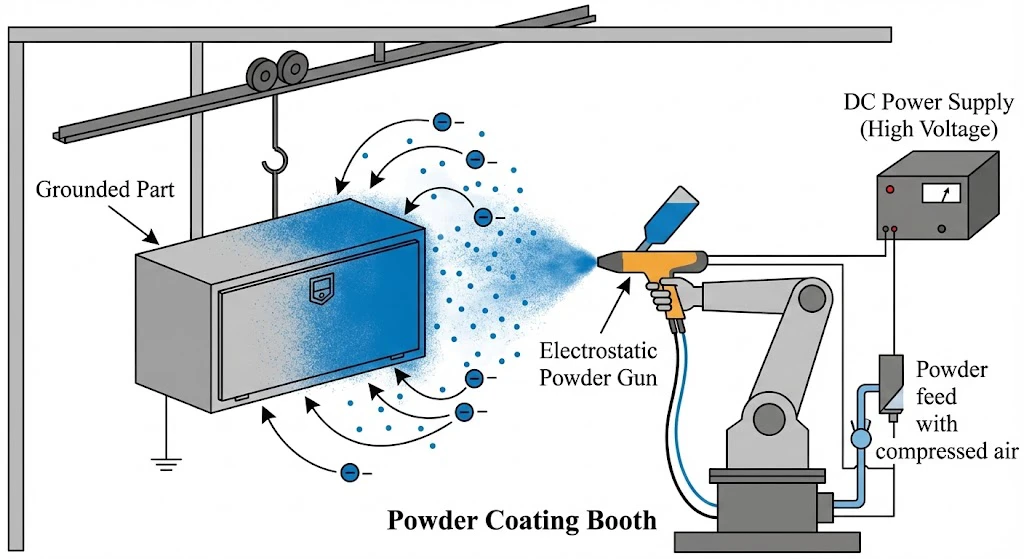
    (C) Electrostatic Powder Coating

    Diagram showing the electrostatic powder coating mechanism applied to Kales trailer parts, where a spray gun applies charged powder onto a grounded metal component.

    Fig 2: Electrostatic powder coating mechanism principles.

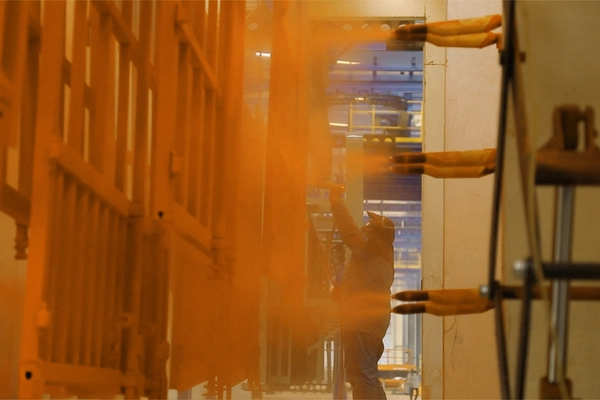
    Automated electrostatic powder coating applied to Kales flatbed semi-trailer components after e-coat, providing durable, zero-VOC finish on visible parts like side rails and toolboxes.
    Kales flatbed trailer parts receiving powder coating after e-coat for long-lasting, eco-friendly surface protection.
    • Principle: Negatively charged powder is sprayed onto a grounded workpiece, then melted and cured at 180–200℃.
    • Core Advantages:
      • Zero VOCs: Compliant with strict national and international environmental laws.
      • High Efficiency: >98% utilization (overspray is recycled).
      • Dense Coating: One-pass application, no sagging (runs), no pinholes from solvent evaporation.
      • Mechanical Strength: Impact resistance ≥50 kg·cm, excellent stone-chip resistance.
    • ⚠️ Thickness Control: Optimal thickness is 60–100μm.Note: Excessive thickness (>120μm) makes the coating brittle, prone to cracking under impact, and causes severe “orange peel.”
    • Resin Types:
      • Epoxy: Strong adhesion but poor UV resistance (Inner parts only).
      • Polyester (TGIC/HAA): Excellent weatherability, suitable for outdoor visible parts (Box bodies, fenders).

    IV. Construction Standards & Acceptance Criteria

    (A) Surface Preparation: The Foundation (70% of Quality)

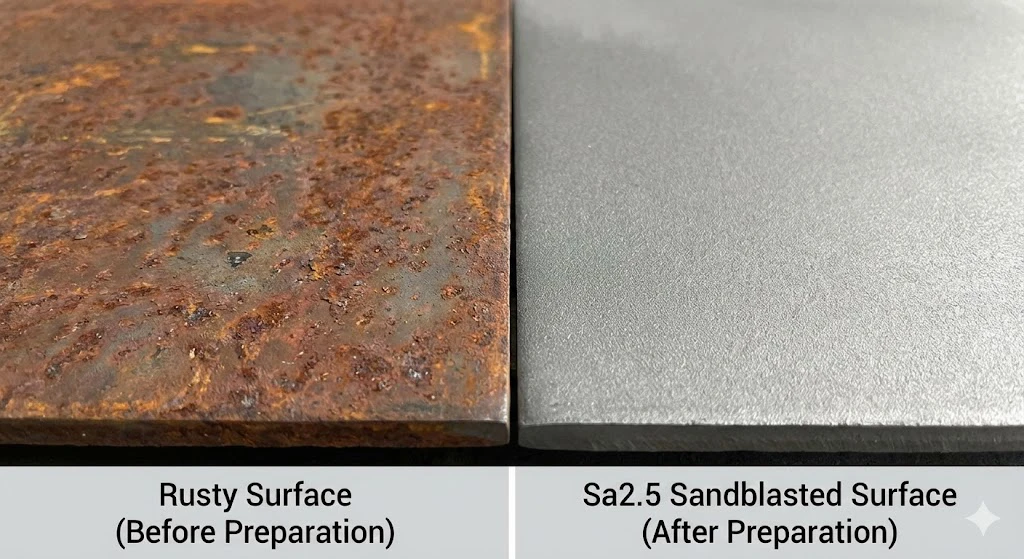
    Side-by-side comparison of a rusty steel surface and the clean, silver-grey Sa2.5 sandblasted surface standard strictly followed by Kales Vehicle.

    Fig 3: Rusty surface vs. Sa2.5 sandblasted surface (The Kales Standard).

    • Manual Brushing: St2 (Visual removal of floating rust) → Not Recommended.
    • Standard Spray/Powder: Sa2.5 Sandblasting (GB/T 8923.1). The surface must present a uniform metallic luster with a roughness of Rz=40–70μm (to increase anchor points).
    • E-coat: Degreasing → Phosphating → Multi-stage Pure Water Rinsing (Cleanliness ISO 8502-9 Class 2).
    • Aluminum Parts: Must undergo Chrome-free conversion (e.g., Zirconium/Silane) or compliant chromating. Simple acid washing or standard phosphating is strictly prohibited.

    (B) Thickness Standards (Reference QC/T 934-2013)

    Process Primer Intermediate Topcoat Total DFT
    Standard Spray Epoxy Zinc (60μm) Epoxy Iron (60μm) PU (50μm) ≥170μm
    E-coat + Baking E-coat (20-25μm) Epoxy (40-60μm) Baking (40-50μm) ≥110μm
    Powder Coating — — Polyester (60–100μm) Single Layer

    💡 Key Insight: Why is “thinner” Powder/E-coat better?

    Quality is not just about thickness, but about density and cross-linking degree. High-temperature cured powder or E-coat forms a molecular cross-link density far higher than air-dried liquid paint, effectively blocking water and oxygen penetration even at lower thicknesses.

    V. 7 Major Paint Failure Risks (Deep Analysis)

    🔴 Risk 1: Poor Surface Prep = Adhesion Loss

    Mechanism: 70% of adhesion relies on substrate surface status. Oil, scale, or insufficient roughness prevents anchoring.
    Symptoms: Blistering, peeling sheets (especially at welds); Cross-cut test fails (≥ Grade 2); Red rust within 48h of salt spray.
    Prevention: Mandate Sa2.5 Sandblasting; Use white gloves to check cleanliness upon delivery.

    🔴 Risk 2: Wrong Primer = No Electrochemical Protection

    Mechanism: Zinc-rich primers protect steel sacrificially. If zinc content is low (<60%) or cheap iron-red primer is used, electrochemical protection is lost.
    Data: Genuine Zinc-rich (≥80%) resists salt spray >500h; Fake Zinc-rich (<40%) rusts in 72h.
    Prevention: Contract must state “Dry Film Zinc Content ≥80%” and demand lab reports.

    🔴 Risk 3: Improper Curing

    Symptoms: Baking paint chalks in 6 months; Powder coating cracks (over-baked) or peels (under-baked); E-coat rusts early due to thinness in cavities.
    Prevention: Factories must use Oven Temperature Trackers to verify the curing curve; Powder must be stored dry (<60% humidity).

    🔴 Risk 4: Incompatible Coating System

    • Typical Error A: E-coat primer + Topcoat without sanding/intermediate coat. Result: Topcoat peels off the slick E-coat.
    • Typical Error B: Aluminum + Zinc-rich primer. Result: Major Mistake! Zinc cannot protect aluminum and causes a saponification reaction, leading to total detachment.

    Solution: Use Epoxy Iron Cloud intermediate coats (wet-on-wet) for steel; Specialized Epoxy primer or direct Polyester powder for aluminum.

    🔴 Risk 5: Design “Dead Zones”

    Problem: Closed beams without drain holes (water accumulation); Gaps between cross members (capillary action).
    Prevention: Drill Φ8–10mm drain holes in closed beams; E-coat solves cavity issues; Standard trailers need internal cavity wax.

    🔴 Risk 6: Severe Environment

    Problem: Northern regions (snow melt agents), Coastal (salt spray), Mining (acidic dust).
    Recommendation: Mandatory E-coat + High DFT (≥160μm). Regular chassis washing.

    🔴 Risk 7: Improper Use & Maintenance

    Mistake: Using high-pressure water guns directly flushing weld seams. Ignoring scratches.
    Correct Practice:

    • Use low-pressure water and neutral detergents (pH 6-8) for chassis cleaning. Avoid strong acids/alkalis that destroy the paint’s cross-linked structure.
    • Crucial: Small area scratches must be spot-repaired immediately using zinc-rich touch-up paint to prevent rust spread.
    • Perform annual inspections of key stress points.

    VI. Material-Specific Recommendations

    Material Recommended Process TABOO (Do Not Do)
    Carbon Steel (Q355/Q700) E-coat + Liquid Baking (Chassis)
    Powder Coating (External Parts)
    Avoid acid wash instead of sandblasting.
    Aluminum Alloy Chrome-free Prep + Polyester Powder
    OR Zirconium + Specialized Paint
    Strictly No Zinc-rich primers.
    No direct E-coat (requires special process).
    Stainless Steel Usually unpainted.
    If needed: Adhesion Promoter + Topcoat.
    Avoid sanding that destroys the dense passive film.

    VII. Lifespan & ROI Analysis (Real Data)

    System 5-Year Status 10-Year Status Est. Life
    Manual Alkyd Major Rust Structure Loss >30% ≤6 Years
    Standard Spray Local Floating Rust Weld Corrosion 10–12 Years
    E-coat + Baking Almost No Rust Minor Topcoat Aging 15–18 Years
    Powder Coating No Fading/Peeling Intact 12–15 Years
    💰 The Economics (Case Study):
    In 2018, a mining fleet in Zambia purchased 50 trailers with the Kales E-coat chassis system. After 5 years of operation in a highly acidic mining dust environment, the structural rust rate was less than 2%. This saved the customer approximately $45,000 in secondary sandblasting and repainting costs.E-coat + Baking paint may cost $1,200–$1,800 more per trailer initially compared to standard spray, but it extends service life by 5+ years and significantly increases resale value.

    Export buyer note: Africa, mining and port corridors

    For African fleets, paint failure usually starts at welds, cross-member joints, landing gear brackets, rear bumpers, mudguard supports, and the underside of the main beam. These areas receive stone impact, mud retention and repeated washing. A buyer should therefore inspect the hidden zones, not only the outside side rail.

    If the trailer will operate near ports, mines, fertilizer cargo, wet clay or salted roads, specify the coating system before price negotiation. The lower quotation may simply remove blasting time, reduce primer quality or skip cavity protection. Those savings are small compared with frame repair, downtime and resale-value loss.

    VIII. Buyer’s Checklist: “Four Looks, One Ask”

    1. Look at the Inner Cavity: Is it a uniform gray/black? (Sign of E-coat; spray guns can’t reach here).
    2. Look at Box/Parts Coating: Is the edge wrapping complete and thick? (Sign of Powder Coating).
    3. Check Hardness: Scratch lightly with a key. No mark? = Baked/Powder. Deep white scratch? = Air-dried paint.
    4. Check Welds & Edges: Is there full coverage? Manual paint often leaves “shadow zones.”
    5. ASK DIRECTLY:
      • “Is the chassis fully immersion E-coated?”
      • “Is the aluminum pre-treatment Chrome-free?”
      • “Is powder thickness controlled under 100μm?”
    ⚠️ Warning: Beware of “Mirror-Finish” New Trucks. Excessive polishing is often done to hide insufficient roughness or orange peel. True industrial corrosion protection values uniformity over mere reflection.

    Conclusion: Paint is the “Invisible Brand” of Quality

    Today’s semi-trailer painting has gone far beyond aesthetics. E-coat protects the chassis safety line, Baking Paint offers high-end texture, and Powder Coating delivers green durability.

    Choosing the right paint isn’t about finding the “most expensive” option, but matching the system to your operating environment. A highway logistics van requires a different strategy than a mining dump trailer.

    At Kales Vehicle, we adhere to a “Customized for Application” philosophy:

    • ✅ No Blind Upgrades: Precise powder thickness control avoids brittleness.
    • ✅ Scientific Protection: We prevent rookie mistakes like using zinc primer on aluminum.
    • ✅ Transparent Delivery: From material selection to thickness reports, complete transparency.

    “Check the paint before you buy the truck. Good paint is worth its weight in gold.”

    With the same steel quality, a scientific anti-corrosion system—Chassis E-coat, Body Powder, Scientific Prep—is what defines a truly high-end semi-trailer.

    Coating acceptance gate: surface, DFT, edges and repair method must be checked together

    A semi-trailer paint system should be accepted by evidence, not by gloss. The buyer should check four layers of proof: surface preparation before primer, dry-film thickness (DFT), edge and weld coverage, and the repair method for transport damage. This is critical for export trailers because corrosion usually starts at brackets, weld toes, beam undersides, bolt holes, landing gear mounts and areas hit by stones or road salt.

    The inspection logic can be anchored to public standards. ISO 8501-1 defines visual cleanliness grades for steel surface preparation, ISO 12944-1 frames corrosion protection of steel structures by protective paint systems, and ISO 2808 covers paint film-thickness determination. These references do not replace the supplier’s coating specification, but they give the purchasing team a clear acceptance language.

    Documents to request

    • Surface-preparation report or photos before primer.
    • Coating system sheet: primer, KTL/e-coat, powder or liquid topcoat.
    • DFT readings on main beams, cross members, brackets and repaired zones.
    • Oven curve or curing record for baked paint or powder coating.

    Block acceptance if found

    • No proof of Sa 2.5 or equivalent blast-cleaning before coating.
    • Thin DFT on edges, welds, brackets or beam undersides.
    • KTL/e-coat exposed outdoors without UV-resistant topcoat.
    • Touch-up paint applied over dust, oil, rust or transport scratches.

    For African ports, mining roads, humid coastal areas and long inland corridors, the coating system must be selected around the failure mode. Mud and stone impact need edge coverage and repair discipline; coastal humidity needs stronger corrosion categories; and mining fleets need easy inspection after each maintenance cycle. A documented acceptance gate gives the buyer a repeatable way to compare suppliers beyond a shiny finished surface.

    Appendix: 2026 Coating Selection Guide (Kales Logic)

    Customer Need Recommended Solution Kales Service Feature
    Economy Logistics (Short haul/Inland) Sa2.5 Sandblast + Epoxy Zinc + PU (DFT≥160μm) Strict material standards, refusing “shiny surface” traps.
    Efficient Long-Haul / Cold Chain Full Chassis E-coat + Intermediate + Baking Paint Provides coating test reports, supports 3rd party inspection.
    Environmental Priority / Export Chassis E-coat + Body Powder Coating Zero VOC process, meets international certifications.
    Aluminum Upper Body Users Chrome-free Prep + Polyester Powder Specialized prep + Weather-resistant formula to avoid galvanic/saponification issues.

    Don’t Let Bad Paint Eat Your Profits

    Tell us about your fleet’s operating environment. Kales engineers will customize the optimal anti-corrosion system and provide a precise quote within 2 hours.

    * Free consultation. Factory direct pricing. No middlemen.

    Need help applying this guide?

    Share your trailer type, payload, routes, operating climate, and photos with Kales. Our team can review the key points from this guide and recommend a practical specification for your fleet.

    1. Send photos of your tractor, trailer, or current component layout
    2. Confirm payload, road conditions, gradients, climate, and duty cycle
    3. Receive a specification or maintenance recommendation within 24 business hours

    Email: jennylee@kalestruck.com  |  WhatsApp: +86 131 5638 8843  |  Request a quote

  • Semi-Trailer Chassis Material Selection Guide: Q345B, Q355B and T700

    Semi-Trailer Chassis Material Selection Guide: Q345B, Q355B and T700

    Published: December 30, 2025 | Last updated: May 30, 2026

    From GB to ASTM Standards: Building a Defense Line for Safety, Cost-Reduction, and Compliance

    Based on the latest GB/T 1591-2018 standards and real-world failure analysis, this guide provides a complete technical framework for international fleet managers to procure high-quality semi-trailers from China.

    📖 Technical Index

    • 1. Industry Evolution: High-Tensile Steel
    • 2. Steel Selection Radar: Key KPIs
    • 3. Detailed Comparison: Q345B vs. T700
    • 4. Weight Reduction Engineering & Math
    • 5. Risk Mitigation: 5 Major Failures
    • 6. Aluminum & Stainless Steel Specs
    • 7. Non-Metal: Flooring & Composites
    • 8. Joints: Welding, Huck Bolts & Sealants
    • 9. Global Standards Cross-Reference
    • 10. ROI Analysis: Total Cost of Ownership

    Technical basis and scope

    How this material guide is supported

    This guide is based on Kales trailer design practice, existing chassis material data in this article, and recognized structural material and welding references. The comparison of Q345B, Q355B and T700 focuses on yield strength, tensile strength, fatigue behavior, weldability, corrosion protection and payload economics because those are the factors that change fleet cost after delivery.

    The standards basis includes GB/T structural steel grades used by Chinese trailer factories, ASTM A572-type high-strength low-alloy steel concepts, EN 10025 structural steel practice, AWS D1.1 structural welding principles, ISO 15614 welding procedure qualification logic, and ISO 12944 corrosion-protection thinking. A buyer should not treat a steel grade name as a complete specification. The purchase contract should also define mill certificate requirements, chemical composition, plate thickness, welding consumables, NDT or visual inspection scope, coating system and repair rules.

    • Use this guide for: flatbed trailers, lowbed trailers, container chassis, dump trailers, tanker chassis and other welded steel structures.
    • Ask suppliers to prove: mill certificate, steel heat number, plate thickness, welding procedure, main-beam design and coating method.
    • Do not buy by steel grade alone: high-strength steel helps only when the section design, welding and anti-corrosion process are controlled together.

    I. Introduction: Material Breakthroughs in Manufacturing

    Selecting the right semi-trailer is a system engineering challenge that combines mechanics, metallurgy, and economics. The manufacturing sector is undergoing a profound transformation:

    • Steel Upgrades: A complete transition from older Q345 to Q355 High-Strength Low-Alloy (HSLA) steel; Q700 (700MPa) is standard for lightweighting, while BST1500 dominates the wear-resistant sector.
    • Material Diversification: Aluminum alloy extends beyond tankers to fuel and food-grade transport; Stainless steel expands to corrosive solid transport.
    • Globalization: Designs are now strictly benchmarked against ASTM (USA) and EN (Europe) standards for export compliance.

    II. Core Material Systems: The Chassis Foundation

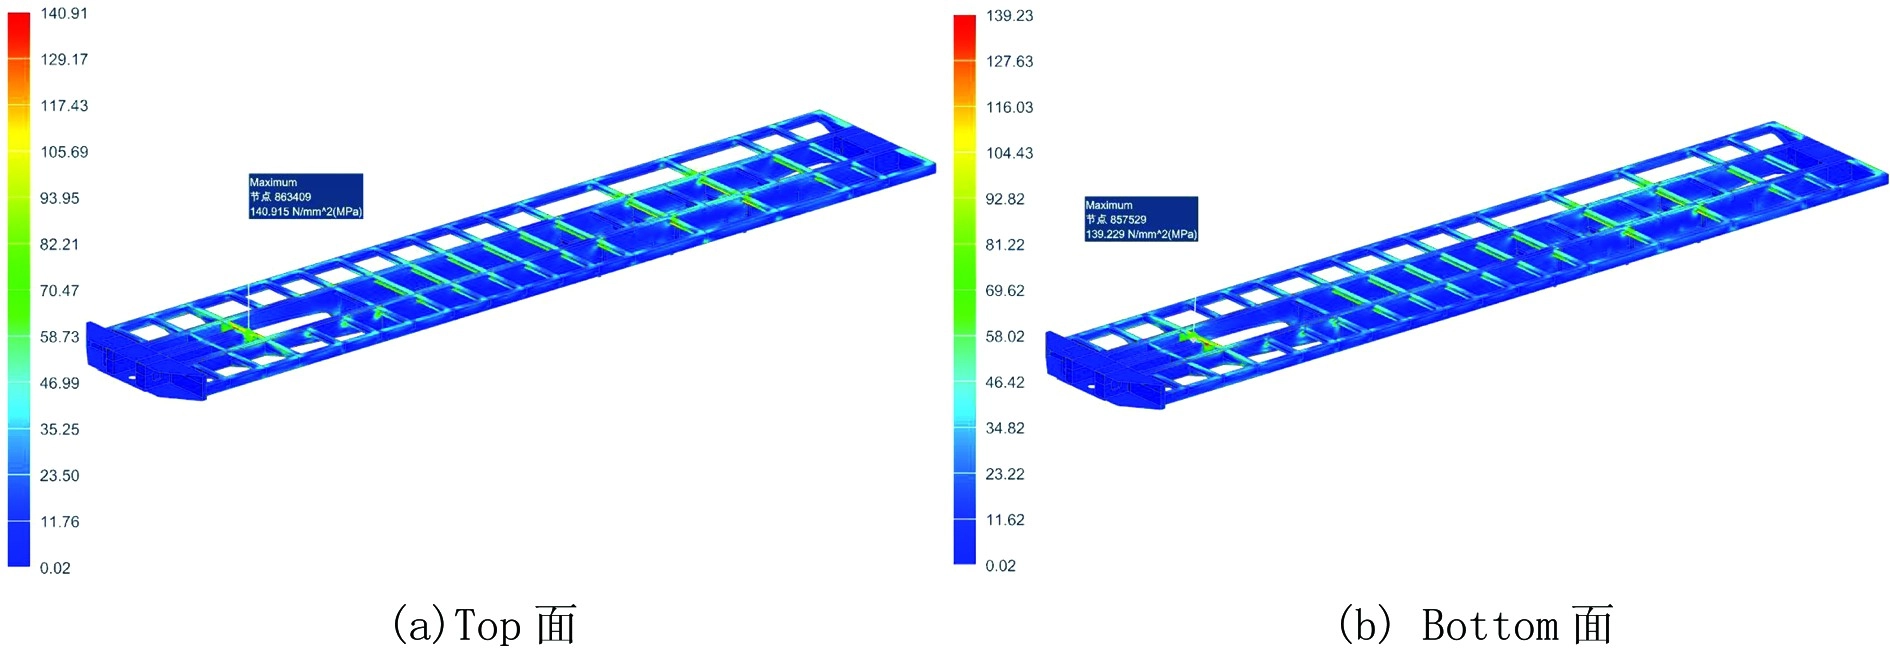
    Finite Element Analysis of Heavy Duty Semi Trailer Chassis Structure Q355 Steel

    Diagram of Semi-Trailer Chassis Structure (Finite Element Analysis Stress Map)

    1. Steel: The Backbone of Your Trailer

    Category Grade Application & Notes
    Mild Carbon Steel Q235B (ASTM A36) Toolboxes, Mudguards. Lowest cost, strictly prohibited for main load-bearing structures.
    HSLA Steel Q355B/C/D/E Main Beams, Cross Members. The industry standard, replacing Q345. Equivalent to S355JR or A572 Gr.50.
    High-Tensile Steel Q700L/E (T700) Lightweight Main Beams (15-30% weight reduction). Superior tensile strength.
    Wear-Resistant Steel BST1500 / NM450 Dump Trailer floors. Hardox equivalent. BST1500 offers ≥1500MPa tensile strength.
    ✅ Regulation Update: GB/T 1591-2018 strictly mandates Q355 over Q345, raising minimum yield strength to ≥355 MPa.

    III. Detailed Comparison: Q345B vs. T700 (Q700L/E) High-Strength Steel

    To optimize trailer weight without compromising structural integrity, manufacturers rely heavily on T700 (Q700L/E) steel for main longitudinal beams. Understanding the mechanical differences between traditional carbon structural steel (Q345B) and high-strength thermomechanically rolled steel (T700) is critical for matching the trailer to the fleet’s duty cycle.

    Property Traditional Q345B (ASTM A572 Gr.50 Equivalent) High-Strength T700 (Q700L/E / S700MC Equivalent) Technical Implications for Fleet Operators
    Yield Strength ($\sigma_y$) 345 MPa 700 MPa (103% Increase) T700 supports double the bending stress before permanent deformation.
    Tensile Strength ($\sigma_u$) 470 – 630 MPa 750 – 900 MPa Prevents catastrophic tearing under extreme overloading or impact.
    Elongation ($A_5$) ≥ 20% ≥ 12% (38% Decrease) Q345B is highly ductile, making it excellent at absorbing dynamic shocks. T700 is stiffer but more brittle.
    Typical Main Beam Profile Upper/Lower Flange: 14/16mm
    Web Plate: 8mm
    Upper/Lower Flange: 8/10mm
    Web Plate: 5mm
    T700 allows for thinner structural plates, leading to significant tare weight savings.
    Fatigue Limit under Dynamic Torsion High fatigue threshold, highly forgiving on rough unpaved roads. Sensitive to weld-toe stress concentrations. Requires post-weld dressing. For severe off-road mining routes, a hybrid design (Q355 chassis with T700 crossmembers) is preferred over a full-T700 chassis.
    Carbon Equivalent (CEV) ≤ 0.44% ≤ 0.48% (Micro-alloyed with Nb, V, Ti) T700 requires strict low-hydrogen welding consumables and preheating to avoid cracking.

    IV. Weight Reduction Engineering & Math

    Reducing the tare weight of a semi-trailer directly increases the payload capacity, which is governed by local gross vehicle weight (GVW) limits. However, downsizing steel thickness must be calculated precisely to ensure the beam does not fail under vertical load or buckle under lateral forces.

    4.1. The Section Modulus Formula

    The load-bearing capacity of the main I-beam is determined by the maximum bending moment it can withstand ($M_{max}$):

    $M_{max} = \sigma_{allow} \times Z_x$

    Where:

    • $\sigma_{allow}$: The allowable design stress of the material, which is directly proportional to its yield strength ($\sigma_y$).
    • $Z_x$: The section modulus of the I-beam, determined by its geometry ($Z_x \approx \frac{1}{6}(b \cdot h^2 – \frac{b_1 \cdot h_1^3}{h})$).

    By upgrading the material from Q345B ($\sigma_y = 345$ MPa) to T700 ($\sigma_y = 700$ MPa), the allowable stress is effectively doubled. Consequently, to maintain the same load capacity ($M_{max}$), the required section modulus $Z_x$ can be reduced by approximately 40%. This geometric reduction is achieved by thinning the flanges and web plates, reducing the steel volume and mass.

    4.2. Fleet Sourcing ROI Calculation Example

    Consider a standard 3-axle 40ft Flatbed Trailer. Let’s compare a traditional Q345B structure and a lightweight T700 structure:

    • Chassis weight in Q345B: 6,800 kg
    • Chassis weight in T700 (Lightweight flanges & webs): 5,600 kg
    • Tare Weight Savings: 1,200 kg (1.2 Metric Tons)
    • Increased Payload: +1,200 kg per trip

    Financial Return (TCO Analysis):
    For a fleet hauling regional freight over 100,000 km per year, assuming a transport rate of $0.08 per ton-km:
    $$\text{Annual Extra Revenue} = 1.2 \text{ tons} \times 100,000 \text{ km} \times \$0.08/\text{ton-km} = \$9,600 \text{ per year}$$
    If the upfront price premium for the T700 trailer is $1,800, the payback period is less than 2.3 months. Over a 5-year operating life, a single trailer yields $46,200 in additional net profit.


    V. Key Technical Indicators for Steel Selection

    The Selection Mantra: “L for Forming, X for Welding; E for Cold Climates, Preheat for 1500.”

    Grade Yield Strength Carbon Equiv. (CEV) Impact Energy (-40℃) Best Use Case
    Q355E ≥355 MPa ≤0.42 ≥34 J Mining & Off-Road. High toughness.
    Q700E ≥700 MPa ≤0.50 ≥34 J Cold Climates (Russia/Canada).
    BST1500 ≥1300 MPa >0.60 Available @ -20℃ Extreme Wear Resistance.

    VI. 5 Major Failure Risks & Prevention Strategies

    Based on real-world failure analysis cases.

    🔴 Risk 1: Cold Brittleness (Brittle Fracture)

    Case Study: A dump trailer using standard BST700L (no impact rating) suffered a main beam fracture at -32°C. Tests revealed impact energy of only 8J (Safe threshold ≥27J).

    Prevention:

    1. Grade Selection: For cold regions, strictly specify Q355E or Q700E.
    2. Contract Clauses: Mandate “Charpy V-Notch Impact Energy ≥27J @ -40°C”.

    🔴 Risk 2: Welding Cold Cracks

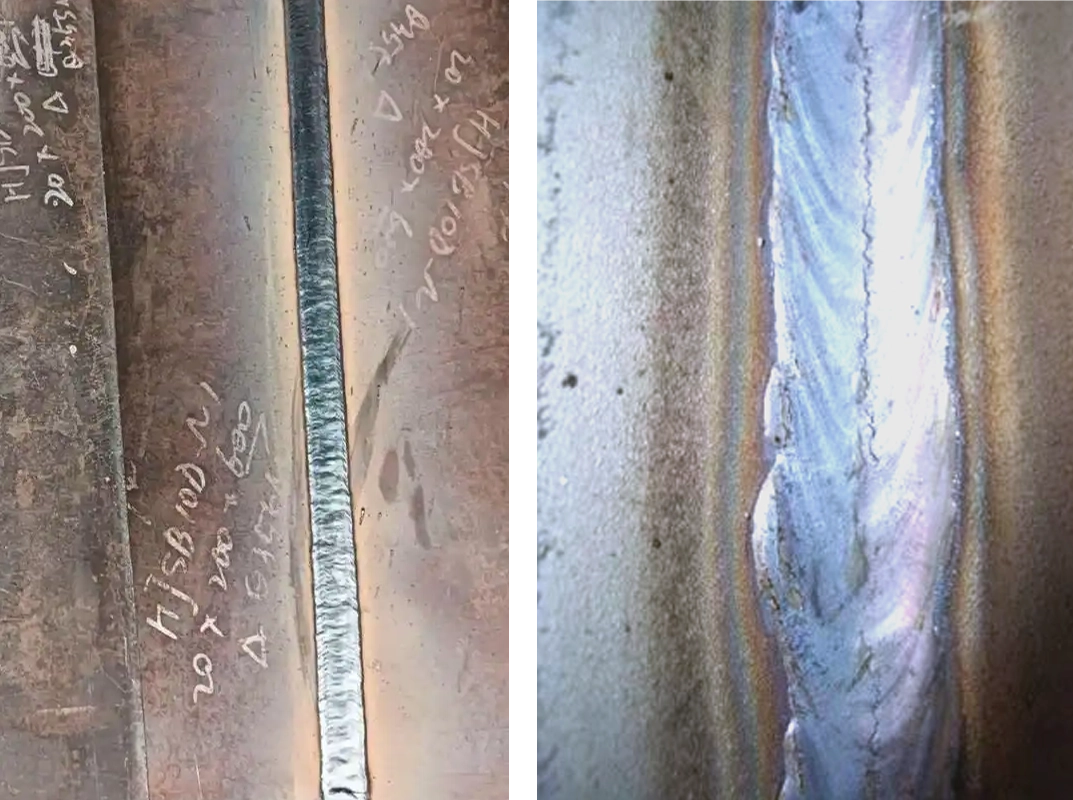
    Microscopic comparison of Healthy Weld vs. Cold Crack in High Tensile Steel

    Microscopic comparison of Healthy Weld vs. Cold Crack in High Tensile Steel

    Root Cause: High tensile steels have high carbon equivalents, leading to hydrogen-induced cracking.

    Prevention:

    1. Pre-heating: Q700 requires 150–200°C; BST1500 requires 200–250°C.
    2. Post-Weld Heat Treatment: Essential for releasing hydrogen.
    3. Inspection: 100% MT/UT testing is non-negotiable.

    🔴 Risk 3: Structural Buckling (Over-Lightweighting)

    Symptom: Chassis distortion on rough roads; “Wavy” buckling of the web plate.

    Prevention:

    1. Minimum Thickness: Web plate thickness should never go below 5mm, even when using Q700.
    2. Design Check: FEA Verification must show first-order modal frequency ≥8 Hz and a safety factor ≥2.0.
    3. Avoid: Do not blindly replace 6mm Q355 with 4mm Q700.

    🔴 Risk 4: Corrosion & Rust

    Prevention:

    1. Surface Prep: Mandatory Sa2.5 Sandblasting (Roughness Rz=40–70 μm).
    2. Coating System: Epoxy Zinc-Rich Primer (≥60μm) + Polyurethane Topcoat.
    3. Coastal Areas: Use Polyurea chassis armor.

    🔴 Risk 5: Counterfeit Materials

    Case: A factory used “HQ700” which turned out to be Q420. The chassis bent within 6 months.

    Prevention:

    1. Source: Buy only from mills with IATF 16949 certification (e.g., Baosteel, Ansteel).
    2. Verification: Request the original MTC (Mill Test Certificate) and cross-check Heat Numbers.
    3. On-Site Test: Perform spectral component analysis + tensile testing upon material arrival.

    Export buyer note: match steel to road, load and repair conditions

    For African corridors, mining sites and long-distance port logistics, the strongest steel is not automatically the best purchase. A high-strength lightweight chassis can carry more payload, but it also requires better welding control and more disciplined overload management. For rough roads, high torsion and driver-side repairs, the supplier should explain how the main beam, cross members and gooseneck are reinforced.

    Before approving a trailer quote, ask whether the proposed steel grade matches the cargo density, road profile, axle load, repair capability and resale market. If the fleet will be maintained far from a professional welding shop, a slightly heavier but easier-to-repair design may be more practical than an aggressive lightweight design.

    VII. Regional Challenges: Andes Terrain vs. West African Corridors

    Steel chasses experience different stress patterns depending on local climates and road profiles. Procuring a standard highway trailer for specialized regional routes will lead to premature structural failures.

    7.1. The Andes Mountain Routes (High-Torsion and Dynamic Shock)

    Fleets hauling copper concentrates or heavy machinery in Peru, Chile, and Bolivia face steep descents, extreme switchbacks, and unpaved mountain roads. Under these conditions, the chassis undergoes severe diagonal torsion (twisting).
    Because Q700 high-strength steel has lower elongation (12% vs 20% for Q355B), it does not flex as well under severe twisting. Continuous twisting leads to high-stress concentrations at crossmember welding joint boundaries, causing fatigue cracking.
    Recommendation: For Andean operations, specify a **heavy-duty Q355B chassis**. While heavier, the high ductility allows the main frame to twist and spring back without cracking. If weight reduction is critical, choose a hybrid design: Q355B for main longitudinal beams and Q700 for non-structural parts.

    7.2. West African Corridors (High Temperature and Corrosive Humidity)

    In West Africa (e.g., Senegal, Côte d’Ivoire, Ghana, Mali), trailers transport cargo from hot, salty coastal ports to hot, dusty inland regions. High humidity combined with sea salt accelerates corrosion, while unpaved roads subject the undercarriage to continuous sandblasting. Underneath, standard paint will chip off, exposing bare steel to salt-rich moisture.
    Recommendation: Mandate **Sa2.5 shot blasting** followed by a two-component **Epoxy-Zinc-Rich primer** and a **Polyurea or Polyurethane topcoat** (total dry-film thickness ≥120 micrometers). Ensure the factory applies anti-corrosion protective wraps over all brake lines and electrical harnesses.


    VIII. Aluminum & Stainless Steel: Applications

    1. Aluminum Alloy (5083/6061)

    • Applications: Tanker bodies (5083-H116), Aviation Fuel (Non-sparking).
    • ⚠️ Galvanic Corrosion: Aluminum and Steel create a battery effect. Solution: Use Rubber/PTFE isolation gaskets; never bolt directly metal-to-metal.
    • ⚠️ Fatigue: Promote Friction Stir Welding (FSW) for 90% joint strength retention.

    2. Stainless Steel (304/316L)

    • Applications: Chemical tankers (316L for acid resistance).
    • ⚠️ Intergranular Corrosion: Always choose Low-Carbon grades (304L/316L).
    • ⚠️ Pickling: Post-weld acid washing (passivation) is mandatory.

    IX. Non-Metal Components: Flooring

    1. Composite Materials (FRP/GRP)

    Top choice for Reefer Trailers. No thermal bridging.

    • Selection Key: The Gel Coat must be UV-Resistant to prevent yellowing. Glass fiber content should be ≥25%.

    2. Flooring Materials

    Container Grade Bamboo China’s Competitive Edge. High strength, water-resistant, and more durable than plywood. Standard thickness: 28-30mm.
    Hardwood (Apitong) The standard for US/European markets. Extreme nail-holding power for securing heavy machinery.

    X. Joint Technology: Welding vs. Mechanical

    Structural integrity depends 30% on material and 70% on connection technology.

    1. Welding Process

    Material Consumables (AWS) Critical Process
    HSLA (Q355) ER70S-6 Standard MAG welding.
    High-Tensile (Q700) ER70-G Must Preheat 100-150℃!
    Wear-Resistant ER50-6 (Base) + ER70-G Preheat 200℃ + Soft wire base layer.
    Aluminum (5083) ER5356 / ER5183 Indoor welding only (Wind protection).
    Stainless (304) ER308L Must be Pickled & Passivated.

    2. Mechanical Fastening: The Huck Bolt

    ✅ The Solution for Steel-Aluminum Joints

    • Why: Steel and Aluminum cannot be welded together due to different melting points.
    • Benefit: Vibration resistance is 5x that of standard nuts/bolts. Permanent locking.
    • Anti-Corrosion: Must use Dacromet coated collars.

    3. Sealing Process (Waterproofing)

    The final defense for keeping cargo dry.

    • ❌ Acidic Silicone: Cheap but releases acetic acid, corroding metal and peeling paint.
    • ✅ MS Polymer Sealant: The industry standard. Solvent-free, UV resistant (10+ years), and paintable.

    XI. Global Standards Comparison Table

    China GB Europe EN USA ASTM Japan JIS Australia AS/NZS Note
    Q235B S235JR A36 SS400 AS3678-250 Mild Steel
    Q355B S355JR A572 Gr.50 SM490A AS3678-350 HSLA Steel
    Q700 S700MC A514 Gr.B – AS3597-700 High Tensile
    5083-H116 EN AW-5083 AA 5083 A5083P AS2747 Marine Alum.

    XII. Total Cost of Ownership (TCO) & Recommendations

    💡 ROI Case Study

    An Aluminum Alloy Box Trailer is 2.2 tons lighter than a steel one. Based on 100,000 km/year, this weight saving translates to significant fuel savings or additional payload revenue. The Payback Period is typically under 6 months.

    Operational Scenario Chassis Material Body Material Tech Requirement
    General Cargo Q355B Corrugated Steel Standard Painting
    Long-Haul Logistics Q700E 5083 Aluminum Huck Bolt Connections
    Fuel/Hazardous Q550 5083 Aluminum Anti-static, Air-tightness
    Mining/Off-Road Q700E BST1500 (Hardox) Pre-heat weld, Chassis Armor

    Material approval gate: MTC, welding procedure and corrosion system must match the route

    A semi-trailer buyer should not approve a chassis by steel grade alone. The release package should connect the mill test certificate (MTC), heat-number traceability, plate thickness, main-beam drawing, welding procedure and corrosion-protection system. Q355B and T700 can both be good choices, but the wrong welding heat input, missing reinforcement detail or weak coating process can erase the advantage of a higher-strength steel.

    Use public standards as a checklist, then adapt them to your market. ASTM A572/A572M is a common reference for high-strength low-alloy structural steel, ISO 15614-1 covers welding procedure qualification, and the ISO 12944 corrosion-protection system helps frame paint-system decisions. These references do not replace local homologation or engineering drawings, but they give purchasing teams a clear evidence checklist.

    Documents to request

    • MTC with steel grade, heat number and chemical/mechanical values.
    • Plate thickness record for main beam, web, flange and high-stress reinforcements.
    • WPS/PQR summary for main beam and gooseneck welds.
    • Paint or KTL/powder process record, including surface preparation.

    Block approval if found

    • Steel certificate cannot be matched to chassis heat numbers.
    • High-strength beam uses generic welding without procedure control.
    • Reinforcement drawing ignores kingpin, suspension and landing-gear stress zones.
    • Local workshop cannot repair the selected material or coating system.

    For export fleets, the best material is the one that fits payload, road torsion, overload discipline and repair access. Andes routes, mining roads, port shuttles and West African corridors do not punish the chassis in the same way. A documented approval gate helps the buyer compare suppliers by evidence, not by a single claim such as “T700 chassis” or “high-strength steel.”

    Conclusion: The “Safety-Longevity-ROI” Trinity

    Modern semi-trailer sourcing is no longer just about price. Q355 offers the best baseline value, Q700 dominates lightweighting, and Aluminum is essential for specialized ROI. Our Advice: Don’t just buy “Steel”—buy the right steel for your specific terrain.

    Need Professional Engineering Support for Trailer Selection?

    Get in touch with Kales engineering to simulate stress loads and determine the optimal steel composition for your fleet’s operating routes.

    Need help applying this guide?

    Share your trailer type, payload, routes, operating climate, and photos with Kales. Our team can review the key points from this guide and recommend a practical specification for your fleet.

    1. Send photos of your tractor, trailer, or current component layout
    2. Confirm payload, road conditions, gradients, climate, and duty cycle
    3. Receive a specification or maintenance recommendation within 24 business hours

    Email: jennylee@kalestruck.com  |  WhatsApp: +86 131 5638 8843  |  Request a quote

  • Ordering a Disc Brake Trailer? Why EBS & Air Suspension Are Non-Negotiable

    Ordering a Disc Brake Trailer? Why EBS & Air Suspension Are Non-Negotiable

    Published: December 27, 2025 | Last updated: May 30, 2026

    In our previous guide, Disc Brakes vs. Drum Brakes: The Ultimate Guide for Fleets, we discussed the superior safety of disc brakes. But here is the hard truth:
    Disc brakes are like high-performance athletes—they need the right equipment to perform. Using them with an outdated suspension or without electronic control is a recipe for premature failure.

    For many fleet owners, upgrading the trailer is the smartest, most cost-effective way to improve safety. But if you tick the box for “Disc Brakes,” you must also tick the boxes for EBS and Air Suspension.

    This isn’t an upsell. It’s about physics, longevity, and protecting your investment. Here is the technical breakdown from Kales Vehicle experts.

    Technical basis and limits

    Why disc brakes should be specified as a system

    A disc brake semi-trailer is not only an axle option. It is a braking-control package made of the disc axle, trailer EBS ECU, modulator valves, wheel-speed sensors, ISO 7638 power connection, load information and suspension behavior. If one part is missing, the trailer may still move, but it will not deliver the stability, pad life or diagnostic value that buyers expect from a premium spec.

    This guide is based on Kales trailer configuration practice, supplier documentation for trailer EBS and air suspension systems, and the electrical interface logic used by ISO 7638 tractor-trailer connections. It is a specification guide, not a legal homologation document. Final selection must still consider local road regulations, tractor compatibility, axle brand, gross combination weight, tire size and route condition.

    Important: stopping-distance numbers in any comparison are affected by tire grip, brake temperature, road surface, load transfer and driver reaction. Use them as decision models, then validate the final trailer with your tractor and route.

    1. EBS: The “Brain” Your Trailer Needs

    🛑 Braking Distance Comparison (EBS Disc vs. Conventional Drum)

    Speed ✅ Vehicles with EBS and Disc Brakes ⛔ Vehicles with Conventional Braking & Drum Brakes Advantage
    50 km/h 25m 30m ↓ 5m shorter
    80 km/h 45m 65m ↓ 20m shorter!
    90 km/h 48m 75m ↓ 27m shorter!

    Conclusion: The faster the speed, the more obvious the advantage of EBS + Disc Brakes.
    At highway speed, the benefit is not only distance; it is earlier, better balanced braking between tractor and trailer. Treat the meter values above as a fleet-spec comparison model, not a universal guarantee.

    You might think: “My driver is experienced, and my truck has standard air brakes. Why pay extra for Trailer EBS?”

    A. The response-time safety gap

    Disc brakes can develop torque quickly, but a pure pneumatic command still has line-fill and valve response delay. EBS reduces that delay by sending an electronic braking request while the air system supplies the force.

    The practical point: the faster the combination and the heavier the load, the more valuable synchronized brake timing becomes. The exact stopping-distance gain depends on tractor condition, tires, axle load, road friction, brake temperature and whether the ISO 7638 EBS power cable is connected.

    B. Coupling Force Control (Anti-Jackknife)

    EBS manages the “Coupling Force” at the kingpin. Ideally, the force between tractor and trailer should be zero.

    Through the ISO 11992 protocol, EBS constantly adjusts the trailer’s braking pressure to ensure it neither “pushes” the truck (Jackknife risk) nor “drags” it. This active stability is impossible with standard air brakes.

    C. The Hidden Bonus: RSS & Wear Control

    • 🛡️ Roll Stability Support (RSS): Automatically brakes specific wheels to prevent rollover on curves.
    • 💰 Wear Harmonization: EBS sensors monitor pad thickness. It reduces pressure on worn pads and increases it on new ones, ensuring all pads wear evenly. This means you can replace all pads at once, reducing service downtime.

    ⚠️ Crucial Warning: The ISO 7638 Cable

    EBS is useless if it’s not plugged in!
    We often see drivers connect the air hoses but forget the ISO 7638 Power Cable (the thick 5-pin or 7-pin spiral cable). Without this connection, your premium EBS is dead, and your disc brakes revert to “dumb” mechanical mode.

    👉 Action Item: Ensure your tractors have this socket functioning and drivers use it.

    2. Air Suspension: The “Bodyguard” for Calipers

    Some buyers think Air Suspension is just for driver comfort. For Disc Brakes, it is a mechanical necessity.

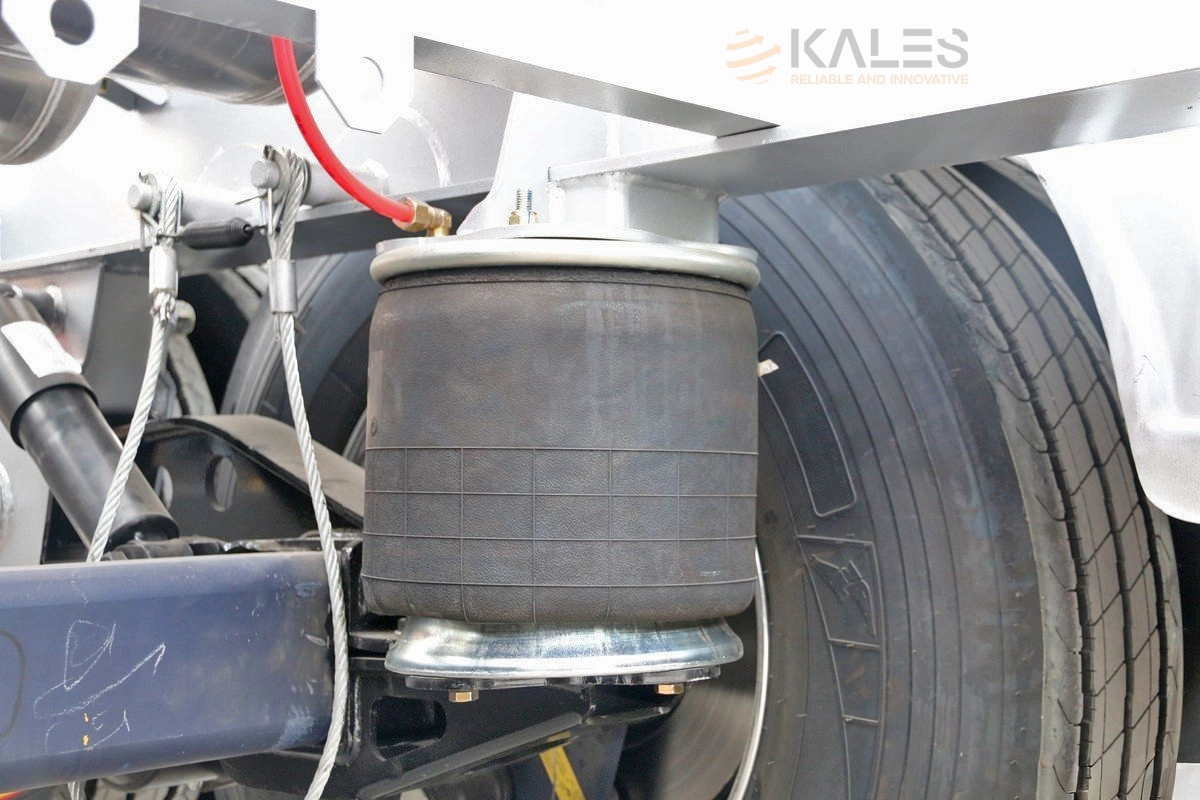
    Air suspension system on a semi-trailer axle that filters road vibrations and maintains constant tire contact with the ground for improved stability and ride comfort.

    Air suspension filters vibration and ensures constant road contact.

    🛡️ 1. Vibration Protection

    The Problem: Steel leaf springs transmit harsh road vibrations directly to the axle. This can shake precise caliper mechanisms loose, causing seizing.

    The Solution: Air bags act as a damper, filtering out vibrations and extending caliper life.

    🛑 2. Eliminating “Wheel Hop”

    Physics: When braking hard on a bumpy road, steel springs make the axle “hop.” A bouncing tire has zero friction.

    The Solution: Air suspension keeps the tire firmly planted on the asphalt, ensuring 100% braking power.

    ⚖️ 3. Load Equalization

    Air suspension instantly equalizes weight across all axles. This ensures no single disc brake is overloaded, preventing rotor cracking due to heat stress.

    3. EBS vs. ABS: What is the Technical Difference?

    Many operators confuse ABS (Anti-lock Braking System) and EBS (Electronic Braking System). While both prevent wheel lockup, their architecture, speed, and safety capabilities represent different generations of technology.

    ABS is a reactive system. It waits for the wheel to lock up during heavy braking, then reduces pneumatic pressure to that wheel. EBS is a proactive system. It controls the braking process from the millisecond the driver touches the pedal, using digital communication to distribute force before wheels can lock up.

    Feature / System Specification Standard Pneumatic ABS WABCO / Kales Electronic EBS Operational Advantage (ROI)
    Braking Signal Method Pneumatic pressure wave (Air line) Electronic pulse (CAN-bus signal) Reduces command delay and gives the trailer ECU a faster, cleaner braking request.
    Response Time 450 – 600 milliseconds 50 – 90 milliseconds Improves repeatability of loaded stops when tires, tractor EBS and trailer brakes are correctly matched.
    Braking Force Control Standard mechanical proportioning valve Dynamic electronic load sensing (EBL) Senses exact payload weight instantly; prevents over-braking of empty trailers.
    Roll Stability Control (RSC) Not available Integrated (Active Rollover Prevention) Senses lateral G-force on curves; applies brakes to prevent rollover.
    System Diagnostic Interface Blink codes or external test port Real-time CAN diagnostics via truck dash Instant sensor alerts; logs mileage, load cycles, and pad wear.
    Wear Control / Balancing Manual adjustment only Electronic Pad Wear Harmonization Ensures even wear between tractor and trailer brakes; extends pad life by 30%.

    4. Air Suspension vs. Leaf Spring: Dynamic Compatibility Analysis

    Combining high-performance disc brakes with traditional leaf spring suspension leads to mechanical issues. Here is why the structural characteristics of the suspension dictate the survival of the brake calipers.

    4.1. The Caliper Vibration Factor (G-Force Acceleration)

    A disc brake caliper is a floating assembly weighing approximately 30-35 kg, containing sliding guide pins, internal adjusting mechanisms, and pneumatic chambers. Traditional multi-leaf steel springs exhibit high internal friction. When an empty or partially loaded trailer travels over rough roads, leaf springs transmit high-frequency shockwaves (exceeding 8G of vertical acceleration) directly to the axle beam.
    This continuous vibration causes the caliper guide pin bushings to wear oval, resulting in caliper twisting, uneven pad wear, and water intrusion past the seals, which leads to caliper seizure. Air suspension, by contrast, isolates the axle from high-frequency shocks, limiting caliper acceleration to less than 1.8G.

    4.2. Brake Torquing & Axle Windup

    Disc brakes generate high peak torque instantly compared to drum brakes. Under emergency braking, this rapid torque application causes the axle housing to twist backward (axle windup). Steel leaf springs flex under this twisting force, changing the axle’s steering angle and causing the trailer to drift.
    Air suspension assemblies utilize robust, rigid trailing arms (often 100mm wide steel forgings) welded directly to the axle tube, which are anchored to the trailer frame by heavy-duty rubber bushings. This rigid trailing arm layout controls axle windup, ensuring the wheels remain aligned even under maximum braking load.

    5. Dynamic Rollover Prevention (Roll Stability Control – RSC)

    Roll Stability Support (RSS) or Roll Stability Control (RSC) is the most critical active safety feature of EBS. A semi-trailer has a high center of gravity. When entering a highway exit ramp or negotiating a curve at excessive speed, the lateral G-force can lift the inner wheels off the road, leading to a rollover before the driver realizes the danger.

    The EBS ECU constantly monitors two critical variables: the trailer’s lateral acceleration (using an internal accelerometer) and individual wheel speeds. If lateral acceleration exceeds a preset threshold (typically 0.35G to 0.40G depending on model configuration) and the inner wheel speed sensors show a sudden drop in wheel load, the EBS ECU takes control:

    1. It bypasses the tractor’s service brake signal, sending a high-pressure air pulse directly to the outer trailer brakes.
    2. It applies heavy braking force to the outer wheels to slow the vehicle down rapidly, reducing lateral force.
    3. It returns the inner wheels to the pavement, stabilizing the trailer and preventing a rollover.

    This automated safety intervention happens in less than 100 milliseconds, often correcting the rollover threat before the driver is aware of the hazard.

    Disc brake trailer ordering checklist

    When requesting a quotation, do not ask only for “disc brake axles.” Ask the supplier to confirm the whole control chain. This avoids a common problem in export fleets: the trailer has premium hardware, but the tractor or harness cannot power and diagnose it correctly.

    Item What to confirm Why it matters
    Trailer EBS ECU, modulators, wheel-speed sensors and diagnostic interface. Controls brake timing, load adaptation and fault reporting.
    ISO 7638 power 24V socket, 7-pin EBS cable, driver connection procedure. Without power, the trailer cannot use the full EBS/RSS functions.
    RSS/RSC Roll stability support activated and matched to trailer type. Helps reduce rollover risk in curves, evasive maneuvers and uneven loading.
    Air suspension Ride-height valve, air bags, shock absorbers and axle load signal. Protects calipers from harsh vibration and improves load sensing.
    Service parts Pad size, rotor type, caliper repair kit and local stock plan. A premium brake package fails commercially if pads and diagnostics are unavailable.

    6. Cost-Benefit Analysis of Premium Upgrade Packages

    Upgrading a trailer specification with disc brakes, EBS, and air suspension represents a higher initial capital expenditure. However, when evaluating the total cost of ownership (TCO) over a 5-year operating period, the savings in maintenance, tire wear, and accident prevention outweigh the upfront cost.

    Cost Category (5-Year Cycle) Standard Spec (Drum + ABS + Leaf Springs) Premium Spec (Disc + EBS + Air Suspension) Net Savings (USD / Trailer)
    Initial Option Price Baseline ($0) +$3,200 (Average upcharge) -$3,200 (Upfront cost)
    Brake Maintenance Labor $1,200 (6 drum relines/adjustments) $350 (2 fast pad replacements) +$850
    Tire Wear Cost $4,800 (12 tires worn prematurely by hop) $3,600 (Air suspension preserves tread) +$1,200
    Fuel Consumption ROI Baseline (High rolling resistance) 1.5% savings (Constant contact) +$1,450
    Accident Risk Mitigation $1,500 (Statistical risk premium) $100 (Rollover/Collision prevented) +$1,400
    Resale Value (5 Years) Baseline resale value Premium configuration bonus +$1,500
    Total Life-Cycle Cost $7,500 $4,300 (Including initial premium) +$3,200 Net Savings

    Where the package pays back fastest

    Disc brakes, EBS and air suspension make the most sense where the trailer is exposed to heat, speed, mixed loading or frequent inspection. African and Latin American export fleets often see all four: port queues, quarry roads, mine access roads, long paved corridors, wet seasons and mountain descents.

    • Long downhill routes: combine EBS diagnostics with driver descent discipline and retarder use; see the Kales downhill braking guide for operational practice.
    • Tankers and high-center loads: RSS/RSC is valuable because rollover risk can rise before the driver feels a severe yaw event.
    • Mixed empty/loaded trips: electronic load adaptation helps avoid aggressive empty braking and weak loaded braking.
    • Dusty corridors: air suspension and proper shocks reduce vibration, while the workshop must still inspect caliper slide pins, ABS sensors and harness clips.

    Configuration release gate: approve EBS, ISO 7638 and air suspension together

    A disc brake trailer should not be released as “disc brake only.” The safer buying decision is a system release gate: the EBS ECU and modulator, wheel-speed sensors, ISO 7638 power line, RSS/RSC function, air suspension ride-height control, axle/brake package, diagnostic tool access and local spare sensors must be approved in one checklist. This is especially important for fleets that mix highway work with ports, job sites, mines or long descents, because one weak interface can cancel the benefit of the premium brake hardware.

    The technical basis is not guesswork. ISO 7638 defines the tractor-trailer electrical connection used by ABS/EBS systems; UNECE Regulation No. 13 sets braking-system expectations for many export markets; and CVSA brake-safety campaign results keep showing why brake condition and diagnostics matter in real fleet inspections. Treat these references as a release framework, then apply the local homologation rules for the country where the trailer will operate.

    Approve before production

    • EBS brand, ECU, modulator and axle compatibility.
    • ISO 7638 socket location, cable route and voltage stability.
    • RSS/RSC parameter file matched to axle count, tire size and suspension.
    • Air suspension ride height, valve position and shock absorber selection.

    Block delivery if found

    • No ISO 7638 connection, damaged plug or unstable warning lamp.
    • Active ABS/EBS fault code after road test.
    • Air suspension cannot hold ride height when loaded.
    • Harness, sensor cable or air hose rubs on the caliper, tire or chassis.

    For the purchasing team, this release gate also improves ROI discipline. It separates a premium disc brake semi-trailer from a trailer that only has premium-looking components. Ask the supplier to hand over the diagnostic report, sensor and harness part numbers, pad/rotor references and tractor compatibility notes before final payment. Those records help the workshop solve future EBS faults faster and prevent a small connector problem from becoming a roadside brake complaint.

    Summary: Calculate Your ROI

    Upgrading your trailer configuration is cheaper than buying a new truck, and it pays for itself.

    Feature The Real Benefit (ROI)
    Trailer EBS 1. Shorter, more repeatable stops: especially when tractor and trailer braking are correctly matched.
    2. Wear Control: Balances pad wear for single-stop maintenance.
    3. Stability: Includes Anti-Rollover (RSS).
    Air Suspension Protects sensitive calipers from vibration damage & prevents tire hopping.
    ISO 7638 Cable Free but Critical. Ensure your drivers plug it in!

    By choosing Disc Brakes + EBS + Air Suspension, you are building a trailer that is safer, lasts longer, and commands a higher resale value.

    Ready to spec your premium trailer?

    Don’t guess. Let Kales Vehicle experts configure the perfect axle and suspension package for your specific road conditions.

    Need help applying this guide?

    Share your trailer type, payload, routes, operating climate, and photos with Kales. Our team can review the key points from this guide and recommend a practical specification for your fleet.

    1. Send photos of your tractor, trailer, or current component layout
    2. Confirm payload, road conditions, gradients, climate, and duty cycle
    3. Receive a specification or maintenance recommendation within 24 business hours

    Email: jennylee@kalestruck.com  |  WhatsApp: +86 131 5638 8843  |  Request a quote

  • Disc Brakes vs. Drum Brakes: The Ultimate Guide for Fleets

    Disc Brakes vs. Drum Brakes: The Ultimate Guide for Fleets

    Published: December 26, 2025 | Last updated: May 30, 2026

    Disc Brakes vs. Drum Brakes on Semi-Trailers: Which Is Safer, Cheaper, and Better for Your Fleet?

    Key Takeaway

    Disc brakes are safer than drum brakes for highway logistics trailers. They respond more predictably with ABS/EBS, resist heat fade on long descents, and provide balanced left-right braking force. NHTSA’s FMVSS 121 rulemaking reduced maximum stopping-distance requirements for many heavy truck tractors by about 30%, but that regulatory benchmark should not be read as a guaranteed disc-versus-drum stopping-distance gain for every trailer. The upgrade costs approximately $5,500 USD more for a 3-axle trailer, but most fleet operators recover that investment within 2 to 3 years through weight savings, reduced tire wear, and lower maintenance downtime. However, drum brakes remain the better choice for mining sites, construction off-road, and severely overloaded operations where mud contamination and raw braking torque matter more than response speed.

    “I heard disc brakes are safer, but they cost thousands more?”
    “Are disc brakes too fragile for heavy loads?”
    “Is the upgrade really worth the investment?”

    In recent years, disc brakes have become a major topic in the global logistics and heavy transport industry. With stricter international safety regulations such as ECE R13 in Europe and FMVSS 121 in North America, more new trucks and premium trailers now come standard with disc brakes. However, many fleet owners still question whether the upgrade is truly justified.

    This guide provides a complete technical breakdown with real cost data to help you make an informed decision.


    What Is the Difference Between Disc Brakes and Drum Brakes on a Trailer?

    Disc brakes use a caliper to clamp brake pads against a rotating disc (rotor), while drum brakes use internal shoes that expand outward against the inner wall of a rotating drum. The clamping action of disc brakes provides faster response and better heat dissipation. The expanding action of drum brakes generates higher raw torque at the same size, making them better suited for extreme off-road conditions.

    Drum Brakes: How They Work

    The brake drum rotates together with the wheel. When the driver applies the brakes, internal pistons push the brake shoes outward against the inner wall of the drum to create friction. Drum brakes offer low initial cost and high braking torque per unit size, which is why they remain the standard choice for heavy-duty off-road and construction transport.

    Kales American-type 13-ton drum brake semi-trailer axle for heavy-duty transport

    Disc Brakes: How They Work

    The brake disc (rotor) rotates together with the tire. When the driver applies the brakes, the caliper clamps brake pads against the disc from both sides to generate friction. Disc brakes are now standard on dangerous goods transport vehicles and high-end logistics trailers worldwide, when the trailer is specified as a complete ECE R13 / ABS / EBS brake package.

    Kales American-type 13-ton disc brake semi-trailer axle for standard freight trailers


    Why Are Disc Brakes Safer Than Drum Brakes for Trailers?

    Disc brakes are safer because they respond faster, resist heat fade, provide equal left-right braking force, and allow visual wear inspection without disassembly. These four advantages make them the preferred choice for ABS/EBS-equipped highway trailers carrying standard or high-value cargo.

    1. Faster Braking Response (Critical for ABS and EBS)

    Disc brakes respond almost instantly, enabling high-frequency braking adjustments. This makes them fully compatible with ABS (Anti-lock Braking System) and EBS (Electronic Braking System). On wet or icy roads, this rapid response effectively prevents jackknifing and trailer swing, according to testing standards defined in ECE Regulation No. 13.

    2. Resistance to Heat Fade on Long Descents

    The drum brake problem: Under continuous braking, the drum heats up and its diameter expands outward. The brake shoes lose contact with the drum surface, causing a dangerous loss of braking force known as heat fade.

    The disc brake advantage: Disc rotors dissipate heat far more efficiently due to their exposed design. Even when a disc expands due to heat, it expands in thickness — pushing closer to the pads, not away from them. This means braking force remains stable and pedal travel does not increase dangerously.

    3. Balanced Left-Right Braking (No Veering)

    Drum brakes have a “self-energizing” effect that can produce uneven braking force between left and right wheels, causing the vehicle to pull to one side. Disc brakes deliver linear and equal braking force on both sides, keeping the trailer stable during emergency stops.

    4. Visual Wear Inspection Without Disassembly

    Disc brakes feature automatic pad-to-disc gap adjustment, reducing manual maintenance labor. Brake pad thickness is visible through the open caliper structure without removing the wheel hub, eliminating the risk of undetected hidden wear that plagues enclosed drum systems.


    How Much Do Disc Brakes Cost Compared to Drum Brakes? (TCO Analysis)

    Upgrading a 3-axle trailer from drum brakes to disc brakes costs approximately $5,500 USD more upfront, but the total cost of ownership is lower over 3 to 5 years. Weight savings, reduced tire wear, and faster maintenance recover the investment within 2 to 3 years for most highway logistics operations.

    Initial Investment

    Upgrade Scope Converting a 3-axle trailer to disc brakes with air suspension adds approximately $5,500 USD to the purchase price.

    How the Investment Pays for Itself

    1. Weight Savings Generate Extra Cargo Revenue

    Disc brake axles are lighter than drum brake axles. A 3-axle setup saves approximately 150 kg of dead weight. Based on 150,000 km per year of operation, this extra payload capacity generates approximately $1,000 USD or more in additional revenue per year. Over 3 years, weight savings alone recover roughly $3,000 USD.

    2. Maintenance Savings Reduce Downtime

    Disc brake pad replacement takes approximately 30 minutes per axle. Drum brake shoe replacement typically requires half a day. Disc brakes combined with air suspension also ensure even tire wear, saving 20% on tire costs across 22 tires per year — equivalent to $800 to $1,200 USD in annual tire savings.

    Disc vs. Drum: 5-Year Cost Comparison

    Cost Factor Drum Brakes Disc Brakes
    Initial axle cost (3-axle trailer) Baseline +$5,500
    Extra cargo revenue (5 years) $0 +$5,000
    Tire savings (5 years) $0 +$4,000 – $6,000
    Maintenance downtime savings Baseline Significantly lower
    5-Year Net Result $0 +$3,500 – $6,500 net savings

    Estimates based on 150,000 km/year highway operation with standard loads. Actual results vary by route, cargo type, and local labor costs.


    When Should You NOT Use Disc Brakes on a Trailer?

    Do not use disc brakes on trailers that operate in muddy construction or mining sites, or on vehicles that are routinely overloaded beyond rated capacity. Disc brakes are also unsuitable for fleets where drivers commonly spray water on hot brakes — a practice that causes thermal shock and disc cracking.

    Limitation 1: Lower Raw Braking Torque at the Same Size

    At the same physical diameter, drum brakes generate higher absolute stopping torque than disc brakes due to the self-energizing shoe effect. For severely overloaded vehicles, this difference matters.

    Solution: Always pair disc brakes with auxiliary retarders or engine brakes. Relying solely on service brakes for heavy descents will cause premature wear on any brake system.

    Limitation 2: Thermal Shock from Water Cooling Will Crack the Disc

    This is the single most common cause of disc brake failure in developing markets.

    • The physics: Brake discs are cast iron. If a disc at 400°C or higher is suddenly doused with cold water, the rapid temperature change causes the metal to contract unevenly. The disc will crack or shatter — an effect called quenching.
    • Mud and debris: On muddy mining sites, gravel trapped in the open caliper acts like sandpaper against the disc surface. For construction and mining operations, drum brakes are the safer and more durable choice.

    Can You Mix Disc Brake Trailers with Drum Brake Tractors?

    Mixing a drum brake tractor with a disc brake trailer is not recommended because the different response speeds create braking lag between the two units. The best combination is EBS + disc brakes on both tractor and trailer. If a mixed setup is unavoidable, a professional technician must adjust the relay valve to minimize response timing differences.

    Tractor-Trailer Braking Compatibility Table

    Tractor Trailer Result
    EBS + Disc EBS + Disc Best — Fully synchronized braking
    ABS + Disc EBS + Disc Good — Minor electronic lag only
    EBS + Disc ABS + Disc Acceptable — Trailer responds slower
    ABS + Drum ABS + Disc Poor — Noticeable response lag
    ABS + Drum EBS + Disc Dangerous — Severe braking mismatch

    How Do You Maintain Disc Brakes on a Semi-Trailer?

    Maintain disc brakes by performing daily visual inspections of the caliper for debris, never spraying water on hot discs, draining air tank moisture every two weeks, and replacing brake pads when friction material reaches 2mm thickness.

    ⚠️ SAFETY WARNING
    Never spray water on hot brake discs — thermal shock will crack the rotor. Always chock all wheels before working under a trailer. Depressurize the air system before servicing any brake component.

    The 3 Rules for Disc Brake Longevity

    • Never water-cool hot discs. Allow discs to cool naturally to prevent thermal shock cracking.
    • Inspect the caliper daily. Check for debris accumulation, visible cracks, or abnormal wear patterns in the open caliper structure.
    • Drain air tanks every 2 weeks. Moisture in the air system corrodes EBS valves and brake actuators, leading to delayed response or failure.

    When to Replace Disc Brake Pads

    Critical Limit: 2mm Minimum Pad Thickness

    Replace brake pads immediately when the friction material wears down to 2mm thickness. Also replace immediately if you observe glazing (shiny hardened surface), visible cracks, or oil contamination on the friction surface.

    Annual Axle Hub Maintenance

    Grease the axle hubs at least once per year to prevent premature bearing failure. For reduced maintenance intervals, consider Kales 13-Ton Disc Brake Axles with factory-applied long-life lubrication.


    Should You Switch to Disc Brakes? Quick Decision Guide

    Your Operation Type Recommended Brake Why
    Highway logistics (standard loads) Disc Faster response, lower TCO, ABS/EBS compatible
    Express and time-sensitive delivery Disc Faster pad changes minimize downtime
    Dangerous goods (ADR/DOT) Disc Often legally required; heat fade resistance is critical
    Cold chain and high-value electronics Disc Cargo value justifies safety premium
    Mining and off-road construction Drum Mud/debris damages open calipers; higher torque needed
    Routinely overloaded vehicles Drum Higher raw braking torque per unit size

    Duty-Cycle Release Gate: When Disc Brakes Pay Back and When Drums Still Win

    Disc brakes are not a universal upgrade; they are a route and maintenance decision. The payback is strongest when the fleet runs long highway corridors, frequent downhill sections, high-value cargo, dangerous goods, cold chain, or EBS/RSS-equipped combinations where fast response and easy visual inspection reduce risk. Drum brakes remain practical where abrasive mud, quarry dust, impact damage, overloading and limited workshop discipline would destroy exposed pads and caliper components.

    The decision should start with regulation and inspection evidence, not only purchase price. FMVSS 121 defines air-brake performance requirements, the NHTSA stopping-distance final rule explains the regulatory push for shorter stopping distances, and CVSA Brake Safety Campaign Results show why maintenance discipline still decides whether any brake package works in the real world.

    • Choose disc first: fuel tankers, refrigerated cargo, express freight, long-descending highways, high-speed corridors and fleets already using EBS/RSS diagnostics.
    • Keep drum first: mining dump, quarry, construction, muddy access roads, chronic overload routes and sites where abrasive debris reaches exposed calipers.
    • Do not approve either system blindly: verify tractor-trailer brake balance, ISO 7638 power, ABS/EBS warning lamps, pad or lining inspection access and local spare-part availability.
    • Use TCO as a release record: compare pad/lining cost, downtime, payload effect, driver training, heat-fade incidents and roadside inspection failures over the same operating route.

    For a complete specification, pair this comparison with the disc brake, EBS and air suspension configuration guide, the ABS/EBS/RSS braking guide, and the semi-trailer brake troubleshooting guide.

    Technical References and Related Kales Guides

    How to use this comparison: treat the TCO figures as a specification worksheet, then verify the final brake package against your local axle load rules, road gradient, tractor ABS/EBS interface and maintenance capacity.

    Frequently Asked Questions About Trailer Disc Brakes

    How often should disc brake pads be replaced on a semi-trailer?

    Replacement frequency depends on operating conditions. For standard highway logistics, front axle pads typically last 100,000 to 150,000 km, and trailer pads last 80,000 to 120,000 km. Fleets that use engine retarders as the primary speed-control device on descents can extend pad life beyond 200,000 km.

    Can disc brakes be installed on a trailer with leaf spring suspension?

    It is technically possible, but air suspension is strongly recommended and often legally required when using disc brakes. Air suspension reduces the vibration transmitted to the caliper mechanism. Excessive vibration from leaf springs can cause premature wear and alignment issues in the precision caliper components.

    Are small cracks on the brake rotor dangerous?

    Hairline heat cracks on the rotor surface are a normal result of thermal cycling during braking and are generally not dangerous. However, if any crack extends to the outer edge of the rotor or is deeper than 1.5mm, replace the rotor immediately. A deeply cracked rotor can fracture under braking force, causing complete brake failure on that wheel.

    What happens if I mix disc and drum brakes between tractor and trailer?

    Mixing disc brake trailers with drum brake tractors creates a braking response mismatch. The disc brakes respond faster than the drums, which can cause the trailer to push the tractor during hard braking. If this combination is unavoidable, have a qualified technician adjust the relay valve timing to reduce the lag between the two systems.


    Need a Specific Trailer Configuration or Quote?

    Our engineering team can calculate the Total Cost of Ownership for your specific routes and cargo profiles.

    📱 Chat with Kales Engineers on WhatsApp

    Need help applying this guide?

    Share your trailer type, payload, routes, operating climate, and photos with Kales. Our team can review the key points from this guide and recommend a practical specification for your fleet.

    1. Send photos of your tractor, trailer, or current component layout
    2. Confirm payload, road conditions, gradients, climate, and duty cycle
    3. Receive a specification or maintenance recommendation within 24 business hours

    Email: jennylee@kalestruck.com  |  WhatsApp: +86 131 5638 8843  |  Request a quote